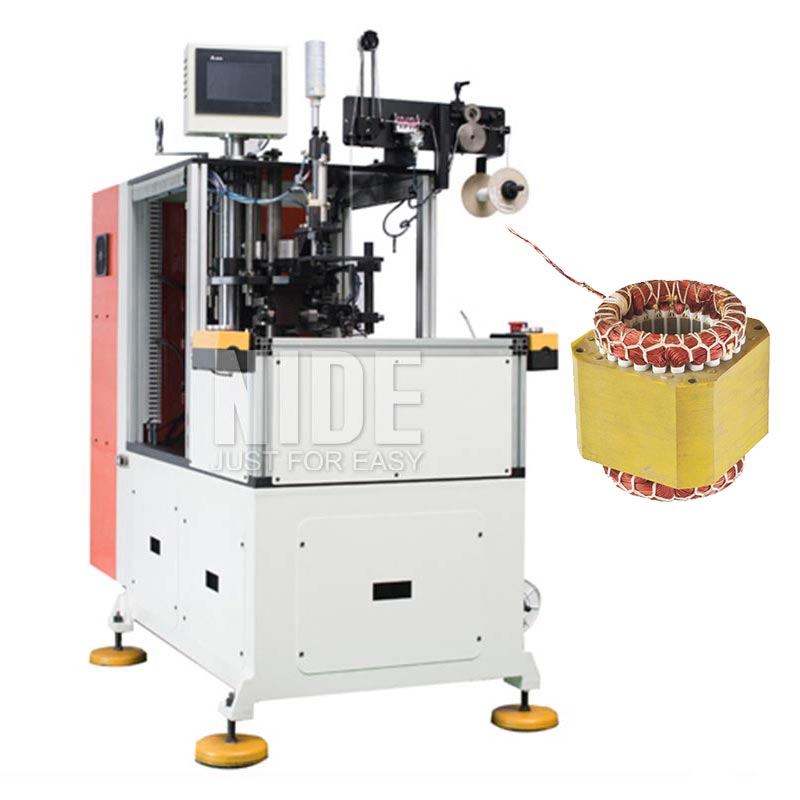
China Best Stator Production Line Manufacturer & Factories Serving Bristol
Turnkey Motor Automation, High-Precision Hairpin Stator Engineering & Tailored Electrification Solutions Engineered for the UK & European Manufacturing Corridors.
Precision Engineering Catalog
High-Performance Stator Lines & Motor Production Equipment
Explore our core turnkey automated machinery, modular inserting systems, and specialized motor accessories manufactured to CE directives and ISO 9001:2015 global standards.
Empowering Bristol's Advanced Engineering Corridor with Advanced Stator Automation
The Greater Bristol area—encompassing the technological vitality of Filton, Avonmouth, Clevedon, and the wider South West Aerospace and Advanced Engineering cluster—has emerged as a focal point for the UK's green industrial transition. From aerospace auxiliary drive electrification to next-generation marine propulsion along the Bristol Channel, engineering teams face stringent targets under UK Net Zero 2050 directives. Achieving high torque density, optimal thermal efficiency, and reproducible electromagnetic characteristics requires transitioning from manual and semi-automated coil assembly to fully integrated, software-synchronized stator manufacturing lines.
As a leading Chinese designer and builder of turnkey motor manufacturing ecosystems, we bridge the gap between capital-efficient manufacturing and Tier-1 European technical criteria. Our stator production lines, incorporating sophisticated PLC-based servo kinematics, high-precision coil winding, slot cell insulation insertion, automatic 3D hairpin bending, and inline surge/hipot testing, provide Bristol's manufacturing enterprises with the operational resilience, cycle-time consistency, and lower total cost of ownership (TCO) demanded in today's competitive landscape.
Aerospace & Defense Auxiliaries
Filton's long-standing aerospace heritage requires extreme electromagnetic integrity. Our specialized needle winding and hairpin stator lines build motors for electro-hydraulic actuators, cabin environment compressors, and auxiliary power units (APU) with minimal slot discharge and Class-H insulation rating.
Partial discharge prevention
Traceable inline electrical testing
Automotive Electrification & Tier-1
Supporting UK EV drive-unit programs, our flat wire hairpin stator assembly lines maximize copper slot fill factors exceeding 70%. High fill factor dramatically cuts I²R copper losses, expanding driving range and matching modern 800V silicon carbide inverter architectures.
Continuous flat wire 3D bending
Vision-guided automated laser welding
Renewable Marine & Industrial Pumps
Bristol Port and Severn Estuary clean energy projects demand ruggedized motor infrastructure. Our high-capacity coil inserting and double-end lacing machines handle heavy magnet wire combinations for high-efficiency IE3/IE4 marine washdown pumps and industrial fans.
Reinforced wedge feeding mechanism
Multi-wire parallel insertion
Engineering Matrix
Traditional Round Wire vs. Automated Hairpin Flat Wire Technology
A quantitative comparison outlining electromagnetic and manufacturing efficiencies to assist Bristol engineering managers in upgrading production lines.
Performance / Manufacturing Attribute
Conventional Round Wire Inserting Line
Advanced Hairpin (Flat Wire) Stator Line
Significance for UK Clean Industrial Hubs
Slot Fill Factor
42% – 48% Average
68% – 76% Max Fill Factor
Drastic volume reduction; enables compact e-axles and aerospace motors.
Thermal Conductivity & Heat Dissipation
Air pockets between round strands hinder heat transfer
Direct face-to-face surface contact with core teeth
Reduces hotspot risks; allows sustained high continuous power outputs.
Automation Repeatability
Moderate; subject to manual cosmetic forming & tying
100% CNC Controlled; robotic hairpin insertion & 3D twist
Full lot traceability conforming to UKCA & European CE machine directives.
Local Market Trajectory: Electrification & The UK Supply Chain Mandate
The United Kingdom's Industrial Decarbonization Strategy and Faraday Battery Challenge highlight an urgent imperative: localized assembly with resilient global equipment backing. For factories in Avonmouth, Emersons Green, and the Severn Beach logistical parks, sourcing production equipment involves striking a balance between machine agility and robust after-sales backing. Our engineering framework supports Bristol operations through:
1. Tooling Modularity: Easily replaceable inserter blades, push fingers, and winding guides tailored for both low-volume prototyping and multi-shift Tier-1 manufacturing schedules.
2. Standardized Western Automation Architecture: Every stator production machine is integrated with industry-standard control systems (Siemens, Schneider, or Mitsubishi PLCs; SMC pneumatics; and Panasonic/Yaskawa servos), ensuring local maintenance engineers in South West England can service machines without specialized overseas intervention.
Why Choose Us
End-to-End Motor Manufacturing Credibility & Operational Rigor
Backing your Capex investments with verified manufacturing excellence, extensive component supply chains, and structured quality control.
ISO 9001 & CE Certified
Operating out of a modern facility spanning over 30,000 square meters, our design, machining, wiring, and assembly processes operate under certified ISO 9001:2015 quality management systems and European CE Machine Directives.
Turnkey System + Component Supply
We supply not just automated machines, but also raw precision components: copper commutators, N52 neodymium block magnets, electrographite brushes, insulation papers, and rotor shafts—providing a consolidated point of warranty and process tuning.
Pre-Shipment Run-Off Protocol
Every stator manufacturing cell goes through rigorous Factory Acceptance Testing (FAT) utilizing your actual laminations, wire gauges, and slot wedges. Full HD video runs and measurement documentation are approved before packing in seaworthy crates.
Addressing essential technical, commercial, and operational queries from UK manufacturing procurement teams.
How do machines accommodate UK 400V 50Hz 3-phase electrical standards?
Every production cell intended for the UK and Bristol industrial sector is custom-configured at the electrical engineering phase. We build internal cabinets natively designed for 400V/415V 50Hz electrical grids, utilizing high-grade Schneider or Siemens breakers, CE-compliant emergency-stop relay architectures, and correct earth leakage protections to ensure seamless integration into your facility without third-party step-down transformers.
What is the typical lead time and shipping route to Bristol (Avonmouth/Royal Portbury Docks)?
For stand-alone semi-automatic stator coil inserting or lacing machines, standard manufacturing cycle time is 45 to 60 days. Fully automated bespoke hairpin or induction motor production lines require approximately 90 to 120 days from CAD drawing freeze. Shipments depart directly from Ningbo Port to the UK—either arriving via Southampton or directly into the Bristol Channel ports (Avonmouth/Royal Portbury) with comprehensive FOB, CIF, or DDP terms.
Can our engineering team run acceptance trials using our proprietary laminations and wire?
Yes, this is an integral part of our standard quality control workflow. We request clients to courier sample lamination stacks, copper magnet wire, slot liners, and wedge material directly to our Ningbo engineering center. We conduct tooling validation, cycle-time verification, and winding resistance/hipot tests on your exact materials before crating. You are invited to join the FAT in person or via live multi-angle interactive video streams.
How is on-site installation, commissioning, and UK technician training handled?
We deploy field service engineers directly to your UK manufacturing location for line positioning, leveling, wiring tie-ins, mechanical alignment, and operator teaching. Concurrently, our lines come equipped with secure remote diagnosis modules, allowing our Ningbo software teams to assist your maintenance crews with PLC code diagnostics, troubleshooting, or parameter adjustments in real time.
Are spare parts and custom winding tooling easily accessible after commissioning?
Yes. All mechanical wear components (inserting blades, wedge pushers, wire cutters, winding needles) are manufactured with high-speed tool steels and given distinct CAD serials. We ship a standard 2-year consumable spare parts package along with each machine. Additional custom tooling sets for new motor models can be rapidly fabricated and couriered via air express to Bristol within 5–7 business days.
Accelerate Your Motor Production Efficiency Today
Looking to set up an advanced stator line, upgrade manual winding cells, or quote custom-tooled automated inserting machines for the Bristol market? Our experienced technical team will evaluate your motor drawings, slot profiles, and target cycle times to supply a turnkey system proposal.