Featured Motor Manufacturing Equipment & Components
Explore our CE certified precision equipment and high-performance materials for automotive armatures, induction stators, and hairpin traction motors.





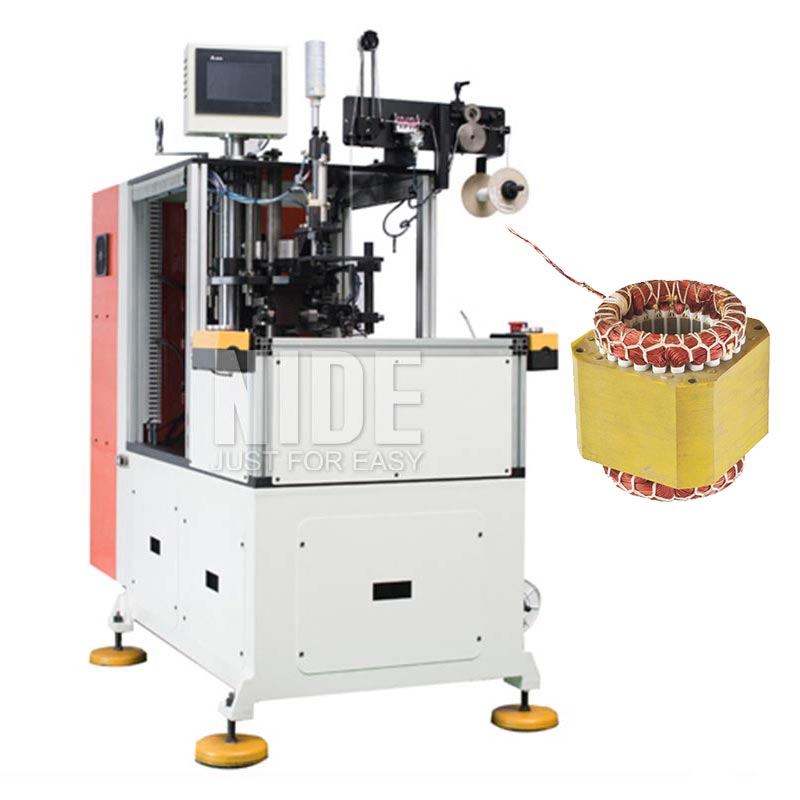


Engineering Whitepaper: Advanced Hairpin Stator Manufacturing Tech
A technical analysis on rectangular copper wire winding, thermal dissipation advantages, slot fill maximization, and production cycle optimization for EV traction drives.
1. The Paradigm Shift: Round Wire Inserters vs. Rectangular Hairpin Technology
In the evolving landscape of electric vehicle (EV) powertrains and industrial high-torque electric motors, traditional round wire stator winding methods are rapidly reaching their thermodynamic and physical limits. Hairpin stator winding technology (flat rectangular copper wire architecture) represents a quantum leap in electromagnetic design, elevating the stator slot fill factor from a conventional 40%–50% up to an extraordinary 75%–82%.
For electric vehicle manufacturers and automotive supply chains situated around Miskolc and the broader Borsod-Abaúj-Zemplén industrial corridor, adopting hairpin stators directly addresses the core engineering metrics required by modern European OEMs: increased power density, reduced torque ripple, exceptional thermal dissipation, and minimized copper loss ($I^2R$) under heavy electrical loads.
Thermal Dissipation
Flat copper surfaces create direct surface-to-surface heat transfer paths against the stator lamination stack, lowering hotspot temperatures by 15°C–25°C compared to randomly wound round wire coils.
Automated Precision
Eliminates manual wire crossing and insulation damage during slot insertion, achieving repeatable CNC multi-axis bending tolerances within ±0.02 mm.
Volumetric Power Density
Higher slot fill enables motor envelope size reductions of up to 20% while outputting equivalent or superior continuous torque for 400V/800V SiC traction architectures.
2. Fully Automated Hairpin Stator Manufacturing Line Workflow
Achieving automotive-grade repeatability requires a zero-defect automated workflow. Ningbo Nakro Intelligent Equipment designs and integrates turnkey hairpin stator lines that execute eight core mechanical and laser processing stages:
- Enamel Wire Pay-off & Precision Straightening: Continuous feeding of rectangular insulated copper wire from multi-ton reels with active tension feedback, eliminating mechanical stress memory.
- Laser Enamel Stripping: High-speed 3D fiber laser ablation selectively removes the outer polyamide-imide (PAI) / polyimide (PI) insulation layer from the hairpin leg tips without compromising the copper substrate.
- 3D CNC Wire Bending & Pin Forming: Multi-axis servo forming heads bend flat wire into precise "U" or "I" shaped pins with custom crown radius dimensions designed for slot insertion.
- Slot Insulation Paper Pre-insertion: B-stage epoxy or Nomex insulation paper is cut, cuff-formed, and pushed into the lamination stack slots prior to conductor loading.
- Hairpin Matrix Nesting & Insertion: A high-density gripper head collects pre-formed hairpins into a circular matrix and simultaneously inserts hundreds of conductors into the stator slots in a single synchronized stroke.
- End-Twisting & Crown Alignment: Precision mechanical twisting heads expand the projecting wire ends according to the winding pitch schematics, creating identical gaps for welding.
- Vision-Guided Fiber Laser Welding: High-speed 3D galvo scanning lasers with inline coaxial vision systems track wire joint centers, fusing copper pairs into clean, porosity-free electrical joints.
- Trickle Impregnation & Electrical Testing: Environmental varnish trickling followed by induction curing, culminating in 100% inline Hipot, Partial Discharge (PD), and Surge impulse verification.
Turnkey Hairpin Stator Equipment Technical Benchmark Specifications
| Parameter Metric | Standard Hairpin Cell Specification | Heavy-Duty Traction Line Specification |
|---|---|---|
| Stator Outer Diameter (Ø) | 120 mm – 280 mm | 180 mm – 450 mm |
| Stack Height Range | 50 mm – 250 mm | 80 mm – 350 mm |
| Wire Cross-Section Area | 2.0 x 1.2 mm to 6.5 x 3.5 mm | 3.0 x 2.0 mm to 10.0 x 4.5 mm |
| Layers per Slot | 4 / 6 / 8 Layers | 6 / 8 / 10 / 12 Layers |
| Laser Welding Speed | ≤ 1.2 sec per joint (3D Galvo) | ≤ 0.8 sec per joint (Vision-guided) |
| Slot Fill Factor Capacity | Up to 78% | Up to 83% |
| Control System Standard | Siemens S7-1500 PLC / Beckhoff EtherCAT | Siemens Safety Integrated / Industry 4.0 MES |
| Compliance Certification | CE MD 2006/42/EC, LVD 2014/35/EU | CE, ISO 9001:2015, UL Components Ready |
Localized Applications & Market Dynamics in Miskolc, Hungary
Strategic engineering alignment with Central Eastern Europe's rapidly expanding automotive and battery manufacturing nexus.
Miskolc, as the administrative and industrial seat of Borsod-Abaúj-Zemplén County, occupies a pivotal role in Hungary’s transition toward zero-emission vehicle production. Positioned in close proximity to major automotive manufacturing hubs in Debrecen, Nyíregyháza, and Győr, Miskolc has transformed into an advanced manufacturing stronghold specializing in machine building, automotive components, electrical equipment, and battery module supply chains.
As major European vehicle brands enforce stringent supply chain localization requirements under the EU’s Green Deal and Euro 7 standards, tier-1 motor suppliers in Miskolc require production machinery that satisfies several localized operational criteria:
- Seamless Grid & Electrical Integration: Full compatibility with European 400V 50Hz 3-phase power distribution networks, featuring regenerative braking power feedback for reduced factory energy consumption.
- EU Machinery Directive 2006/42/EC Strict Adherence: Every Nakro machine shipped to the Miskolc market carries dual CE certification (Machinery Directive & Electromagnetic Compatibility Directive 2014/30/EU), equipped with Pilz safety relays, dual-channel emergency stop loops, and light curtains.
- Interoperability with Central European MES & Industry 4.0 Protocols: Real-time process data acquisition via OPC-UA, MQTT, and Profinet interfaces, allowing plant engineers in Miskolc to monitor wire tension, welding energy curves, and cycle times directly from centralized control rooms.
- Skilled Technical Workforce Alignment: Intuitive multilingual HMI software interfaces (English/German/Hungarian language options) coupled with standardized Siemens PLC programming frameworks to streamline local operation and maintenance.
Why Tier-1 Manufacturers Choose Ningbo Nakro Equipment
Fourteen years of engineering excellence, robust R&D infrastructure, and reliable overseas service support.
14+ Years Specialized Focus
Founded in 2010 in Ningbo, Zhejiang, operating a modern 30,000+ m² facility dedicated solely to armature, stator, and turnkey motor production machinery.
ISO 9001 & CE Quality Rigor
6-stage internal quality inspection process covering incoming material certification, CNC tooling tolerance checks, electrical cabinet safety testing, and pre-shipment trial runs.
Global Service & Local Partners
Proven export track record across 50+ countries. We provide remote augmented-reality diagnostics, on-site commissioning, operator training, and localized spare parts stocking.
Frequently Asked Questions (Miskolc Buyer Procurement Guide)
Direct answers to technical, regulatory, and commercial queries commonly raised by European automotive procurement directors and plant operations teams.
Q1: How does Nakro ensure CE and safety compliance for machines delivered to Miskolc, Hungary?
Q2: Can Nakro customize hairpin winding and bending tooling for non-standard copper wire dimensions?
Q3: What Factory Acceptance Testing (FAT) and Site Acceptance Testing (SAT) protocols are offered?
Q4: What is the typical lead time and shipping arrangement for a complete hairpin stator line to Hungary?
Q5: How are spare parts, tooling wear items, and post-warranty technical support managed locally?
Ready to Automate Your Motor Production Line in Miskolc?
Send us your stator drawings, copper wire specs, and target annual volume. Our senior sales engineers will provide a comprehensive equipment proposal, plant layout diagram, and quotation within 24 hours.
Inquire Now