Component

High Precision Motor Carbon Brushes CE Certified Model NDPJ-TS-9
Ultra-low wear electro-graphite composition engineered for fractional auxiliary motors and universal drives.
Explore our automated stator assembly lines, specialized needle winders, and critical motor sub-components engineered for high slot-fill density, cycle speed, and zero-defect quality control across European manufacturing setups.
Ultra-low wear electro-graphite composition engineered for fractional auxiliary motors and universal drives.

Precision-slotted copper hook commutator offering thermal resilience for automotive thermal management pumps.

Turnkey industrial cell for slot insulation, multi-spindle winding, and hydraulic coil expansion.

High-speed optical orientation and magnetic insertion for exterior and interior permanent magnet rotors.

Silver-copper alloy segment commutators balancing electrical conductivity and dielectric strength.

Reinforced industrial grade brushes built for marine starter dynamics and continuous duty cycles.

High slot-fill flat rectangular wire forming, continuous twisting, laser stripping, and robotic 3D welding.

Simultaneous wedge cutting and electromagnetic wire insertion preserving enameled insulation.
Understanding the transition from traditional AC induction lines to high-efficiency brushless stator topologies in Central & Southeast Europe.
As Croatia cements its position within the European Union's advanced high-technology corridor—driven by groundbreaking electric powertrain innovation around Zagreb, coastal maritime automation in Rijeka and Split, and regional agricultural machinery modernizations in Slavonia—the manufacturing sector faces strict regulatory pressures. The mandate for IE4 (Super Premium Efficiency) and IE5 (Ultra-Premium Efficiency) standards under Directive (EU) 2019/1781 requires an immediate shift away from low-efficiency asynchronous motors toward precision Brushless DC (BLDC) and Permanent Magnet Synchronous Motors (PMSM).
Building an efficient BLDC stator assembly line demands severe metallurgical and mechanical accuracy. Unlike standard induction motors where coil insertion tolerances can accept slight variation, BLDC architectures require superior copper slot-fill factors exceeding 78%, precise multi-axis CNC needle winding to prevent crossed turns, micro-ohm resistance uniformity across three-phase terminal connections, and low-stress insulation barrier application. Our equipment directly resolves these engineering hurdles through closed-loop servo tension controllers that preserve the dielectric integrity of enamelled copper wire down to 0.05 mm tolerances.
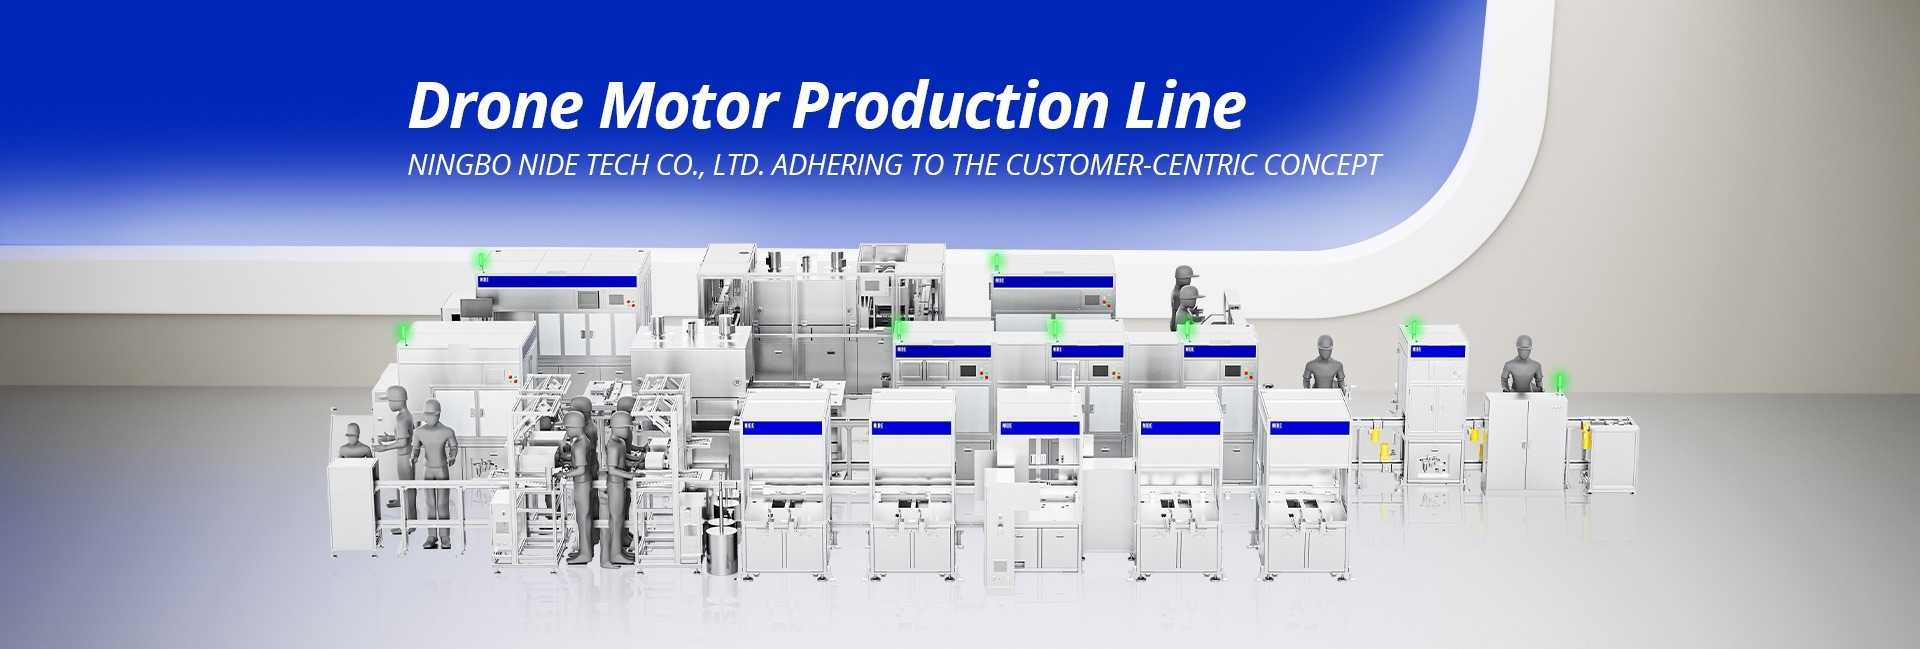
Our complete turnkey BLDC production line addresses each critical production phase, preventing common failure points such as corona discharge, partial insulation breakdown, and thermal bottlenecking:
1. Core Insulation & End-Cap Assembly: Precision pneumatic indexing presses apply high-temperature epoxy insulating end-plates or automatically inject powder-coated insulation along the stator tooth walls, eliminating sharp core burr interference.
2. Multi-Spindle CNC Needle Winding: Utilizes multi-axis synchronized servo systems to direct-wind concentrated coils directly onto internal stator teeth. Programmable continuous wire tensioning prevents elongation spikes that cause premature hot spots.
3. Terminal Lead Management & Hot-Staking Fusing: Automated hook wire manipulation paired with intermediate frequency inverter fusing or fiber laser welding guarantees gas-tight, vibration-immune copper-to-copper terminal connections without flux residue.
4. Vacuum Pressure Impregnation (VPI) & Trickle Varnishing: Uniform resin penetration seals all air pockets between winding layers, optimizing heat transfer to the motor housing while preventing coastal salt-air galvanic oxidation.
5. Comprehensive End-of-Line (EoL) Stator Electrical Verification: Fully integrated computerized testing cabinets run high-potential (Hi-Pot 5kV), surge impulse testing, insulation resistance (>500MΩ), DC winding resistance balancing, and back-EMF phase angle verification in one clamp cycle.
Customized production engineering aligning with Croatian manufacturing clusters from automotive prototyping to Adriatic marine electrification.
With world-renowned electric hypercar engineering rooted in Sveta Nedelja, the demand for precision BLDC and Hairpin stator assembly is exceptionally high. Our lines offer flat copper wire bending, sub-millimeter insertion, and laser welding cells built for high torque-density vehicle powertrains.
Shipbuilding facilities in Pula, Rijeka, and Split require BLDC motor stators that withstand demanding salinity. Our lines integrate automated anti-corrosion varnish dip stations and encapsulation processes tailored for electric catamarans, offshore yachts, and naval ventilation fans.
In line with green tourism infrastructure along the Dalmatian coast, commercial HVAC manufacturers build brushless ECM and BLDC compressor motors. Our needle winding machinery achieves optimal slot fill factors, suppressing torque ripple and acoustic resonance below 35 dB(A).
How Croatian electromechanical factories are modernizing infrastructure to stay competitive in the EU single market.
European supply chain realignments have led industrial buyers in Germany, Austria, and Italy to shift high-precision electric motor sourcing to Croatia. To capture this contract manufacturing volume, Croatian workshops require flexible production machinery capable of switching between 12-slot, 18-slot, and 24-slot stators with quick modular tool changes in under 20 minutes.
In municipal water treatment, commercial refrigeration, and automated agricultural equipment in Osijek and Slavonski Brod, brushed DC machines are systematically being phased out. Brushless stators provide double the operating lifespan without brush degradation or sparking hazards. Our assembly lines empower factories to transition to BLDC production without redesigning their physical floor plans.
Modern production facilities across Zagreb County demand seamless digital manufacturing. Our PLC controllers come equipped with native OPC-UA and Ethernet/IP protocols, providing Croatian plant managers real-time telemetry over winding tension, cycle time, thermal profiles, and 100% cloud-traceable testing archives for ISO auditing.
Proven engineering legacy, ISO 9001 certified quality control, and full-spectrum electromechanical solutions.
Over 14 years of dedicated focus on motor manufacturing machinery, armature cells, and complete automated stator production lines exported to 50+ countries.
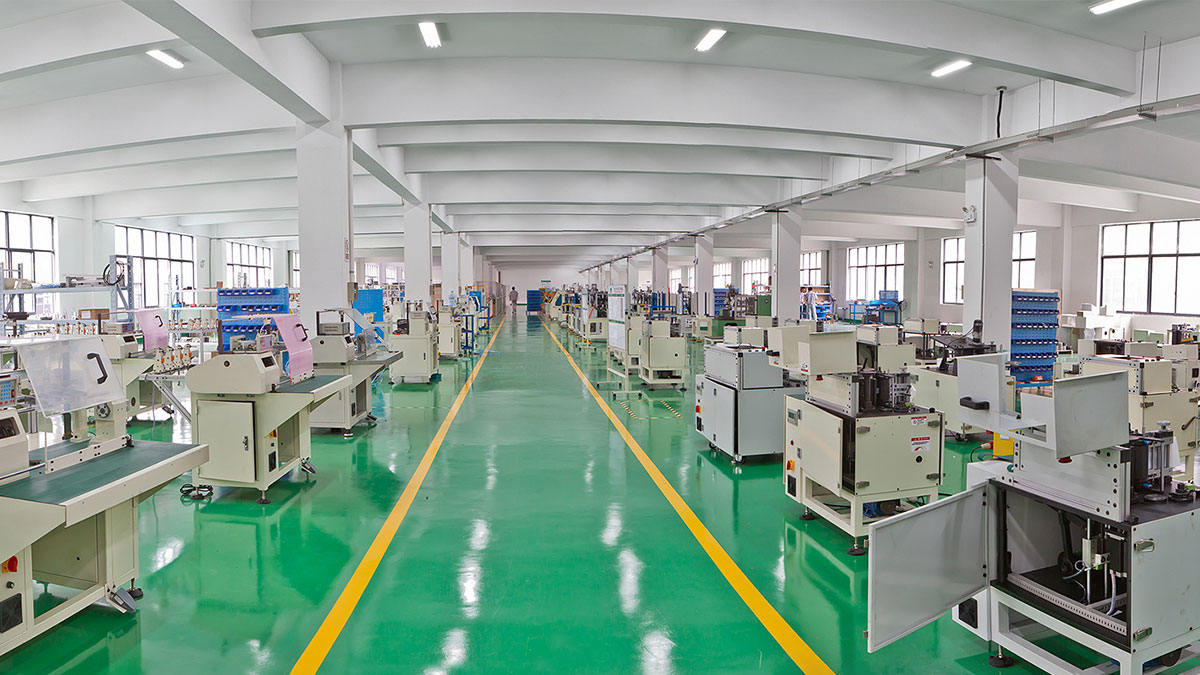
State-of-the-art CNC machining centers, climate-controlled testing laboratories, and high-capacity assembly bays housing over 200 skilled machinery technicians.
Experienced electromechanical engineers design proprietary winding nozzles, expansion blades, and fixtures matched directly to your stator lamination drawings.
One-stop supply capability providing not just automation lines, but matched commutators, carbon brushes, bearings, lamination stacks, and insulation paper.
Clear, technically accurate answers covering import logistics, CE certification, power specifications, and local commissioning in Croatia.
Yes. All machines exported to Croatia and across the European Union strictly conform to CE Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and Electromagnetic Compatibility (EMC) Directive 2014/30/EU. Equipment is fitted with dual-channel emergency stop safety circuits, optical safety light curtains, interlocked protective safety enclosures, and branded electrical hardware (Siemens, Schneider, or Omron).
All electrical panels are custom-engineered for the Croatian national standard grid: 400V AC three-phase (±10%), 50Hz, with neutral and protective ground (TN-S earthing system). All control loops operate on stabilized 24V DC for safety and noise suppression.
We execute a comprehensive Factory Acceptance Test (FAT) utilizing your actual stator lamination stacks, copper wire gauges, terminal clips, and insulation materials. We run continuous batch cycles, record multi-angle 4K run-off videos, provide coordinate measuring machine (CMM) reports for critical tools, and issue complete electrical testing logs. Croatian engineering teams are welcome to attend the FAT either on-site at our facility or via live interactive video conferencing.
With more than 13 years of machinery export experience, we support clients through both overseas service partner networks and direct factory deployment. Our automation engineers can be dispatched to your plant in Croatia for physical uncrating, mechanical alignment, anchor bolting, line commissioning, and hands-on maintenance training. Furthermore, every machine features an integrated industrial VPN modem allowing our software team in Ningbo to perform instant remote PLC diagnostics and firmware updates.
We support standard international commercial terms including FOB Ningbo/Shanghai, CFR, and CIF (Port of Rijeka or Port of Koper). All machinery is treated with rust-preventative VCI coatings, vacuum-sealed in heavy-gauge barrier foil with desiccant bags, and secured in heat-treated ISPM-15 compliant solid wooden cases. Payments are settled in EUR or USD via Telegraphic Transfer (T/T) or confirmed, irrevocable Letters of Credit (L/C).
Yes. Our BLDC needle winding and insertion cells utilize modular quick-change tooling. Stack height adjustments from 10 mm up to 120 mm are managed via digital servo recipes stored on the HMI touchscreen without mechanical disassembly. When changing stator outer diameters, quick-clamp tool holders allow full fixture changeovers in less than 25 minutes.
Send us your motor stator CAD drawings, target annual production capacity, and slot specifications. Our senior automation engineering team will provide a comprehensive project proposal, cycle time calculation, and turnkey line layout customized for your facility in Croatia.
