
Advanced Mid-Drive Motor Assembly Equipment & High-Tolerance Core Components
Explore our core engineering catalog featuring automated coil winders, hairpin stator cells, robotic magnet insertion modules, and high-conductivity copper commutators optimized for mid-drive e-bike, cargo e-trike, and EV traction drives.







Industrial Application Scenarios for Mid-Drive Motor Assembly in San Fernando
The San Fernando Valley and the broader Greater Los Angeles industrial corridor represent North America’s most demanding testbed for light electric powertrains, micro-mobility cargo logistics, and specialized robotic mobility systems.
High-Torque E-Cargo & Last-Mile Delivery Fleets
The San Fernando logistics corridor links major fulfillment centers along I-5 and CA-118 with densely populated Southern California metropolitan districts. Local delivery fleets are aggressively transitioning from rear-hub motors to high-torque mid-drive systems (85 Nm to 160 Nm).
Mid-drive motors utilize the bike’s mechanical gearing to optimize cadence and thermal dissipation during steep grade climbs across the San Fernando foothills, delivering up to 38% higher battery efficiency during start-stop cargo operations.
Premium E-MTB & Urban Performance Mobility
Southern California houses one of the world's most lucrative consumer outdoor enthusiast and premium commuter bike segments. Mid-drive powertrains ensure centralized center-of-gravity, natural torque-sensor responsiveness, and low un-sprung mass on rear suspension setups.
Our automated production machinery enables San Fernando-based OEMs to manufacture lightweight PMSM brushless mid-drive units featuring segmented stator cores, integrated reduction gearboxes, and bilateral torque sensor assemblies with sub-micron runout.
Industrial Autonomous Guided Vehicles (AGVs) & AMR Hubs
Warehousing and advanced manufacturing facilities throughout the San Fernando Valley, Burbank, and Sylmar are deploying autonomous mobile robots (AMRs). These automated systems require heavy-duty mid-drive traction modules capable of 24/7 continuous operation.
Nakro’s automated manufacturing lines assemble industrial-duty BLDC mid-drive actuators with Class H insulation, high-precision stainless steel bearings, and resolver feedback systems rated for over 30,000 duty hours under fluctuating payload stresses.
San Fernando & Southern California Market Trends Driving Mid-Drive Adoption
Strategic manufacturing investments in California are governed by strict environmental directives, decarbonization mandates, and the shift from commoditized imports to localized high-value technical assembly.
CARB Mandates & Clean Fleets Regulation
The California Air Resources Board (CARB) Advanced Clean Fleets (ACF) and commercial zero-emission targets are accelerating the replacement of fossil-fueled utility vehicles with light-duty electric delivery vehicles and commercial cargo cycles.
Mid-drive powertrains provide the high low-end torque needed for utility payloads exceeding 300 kg without overheating electrical windings.
Nearshoring & Local Final Assembly (SKD/CKD)
To mitigate high Section 301 tariffs on fully built Chinese e-bikes and speed up regional responsiveness, San Fernando assemblers are importing Semi-Knocked-Down (SKD) or Completely-Knocked-Down (CKD) motor stator/rotor assemblies.
By establishing localized assembly and testing stations powered by Nakro turnkey cells, manufacturers qualify for regional clean-energy incentives and "Assembled in USA" certification.
Flat-Wire Hairpin Stator Transition
The industry is transitioning rapidly from traditional round-wire winding to rectangular flat-wire hairpin stators. Hairpin technology increases slot fill factor from ~45% to over 72%, dramatically reducing copper losses and overall motor axial length.
Our fully automated EV and e-bike hairpin lines offer high precision CNC bending, automated twisting, and laser welding engineered for compact bottom-bracket integration.
UL 2849 & NFPA Electrical Fire Safety Standards
Following stringent municipal safety legislation across California, e-bike drivetrains and lithium power assemblies must strictly comply with UL 2849 fire and electrical safety standards.
Nakro’s inline assembly cells integrate 100% End-of-Line (EOL) electrical testing stations covering high-voltage hipot testing, inter-turn surge analysis, DC resistance checks, and hall sensor phase synchronization to guarantee complete regulatory conformity.
Engineering Architecture: Complete Turnkey Mid-Drive Motor Production Flow
From bare silicon steel laminations to fully calibrated and dynamometer-verified traction systems, our modular production lines ensure process repeatability, high takt times, and complete quality traceability.
| Station # | Process Module | Key Automation Technologies | Tolerance & Cycle Parameters | Quality Checkpoint |
|---|---|---|---|---|
| Station 01 | Stator Lamination & Insulation | Automatic stack riveting, epoxy powder coating / slot cell paper inserting | Takt: 18-24s; Stack height ±0.05 mm | Optical height sensor, visual surface defect scan |
| Station 02 | Needle Winding / Hairpin Forming | Multi-axis CNC flyer or multi-needle winding; closed-loop servo wire tensioner | Tension accuracy ±0.2N; Wire diameter 0.35–1.6mm | Real-time wire tension logging & turn-count verification |
| Station 03 | Lead Trimming, Fusing & Terminals | Fiber laser striping, pneumatic hook welding / inverter resistance brazing | Weld temperature monitoring ±5°C; Zero spark spatter | Weld nugget shear force verification, contact resistance |
| Station 04 | Stator Impregnation & Curing | Trickle varnishing or vacuum pressure impregnation (VPI) with infrared tunnel | Resin fill rate >95%; Class H/C thermal rating | Dielectric withstand test (hipot >2.5kV AC, surge 3.0kV) |
| Station 05 | Rotor Magnet Insertion & Bonding | Robotic pick-and-place, automated dispensing of two-part structural acrylic | Glue volume repeatability ±0.01 ml; Cycle <20s | Magnet polarity check via hall probe array, glue spread vision |
| Station 06 | Dynamic Balancing & Shaft Press-fit | Dual-plane dynamic balancing unit with automated milling / additive weight | Residual unbalance ≤0.5 g·mm/kg; Press stroke ±0.01 mm | Load-displacement curve analysis during hydraulic press |
| Station 07 | Gearbox & Torque Sensor Marriage | Planetary / helical gear backlash adjustment, bilateral strain-gauge calibration | Backlash ≤12 arcmin; Torque linearity error <1.2% | Torque curve response profiling, low-speed drag torque |
| Station 08 | End-of-Line (EOL) Dynamometer Test | Fully enclosed acoustic anechoic box, regenerative load dyno, back-EMF scanner | Full motor spectrum: 0-12,000 RPM, up to 200 Nm load | Noise vibration harshness (NVH <58 dBA), efficiency map |
Why North American & Global OEMs Partner with Ningbo Nakro
With an operational legacy dating back to 2010, Ningbo Nakro Intelligent Equipment Co., Ltd. combines heavy manufacturing infrastructure with specialized precision automation engineering to support the global electric mobility revolution.
True Turnkey Single-Source Integration
Unlike standard machinery brokers who source sub-assemblies across disconnected third parties, Nakro engineers and builds stand-alone machines, semi-automatic cells, and fully automated lines in-house.
Furthermore, we supply the complete matching component ecosystem: high-precision commutators, 608ZZ stainless bearings, carbon brushes, composite insulation paper, forged shafts, NdFeB magnets, and CNC aluminum motor shells.
Rapid Custom Tooling & Prototyping R&D
Our dedicated engineering department customizes winding nozzles, insertion tooling, clamping mandrels, and dynamic fixture sets directly around customer slot geometries, lamination stacks, and wire configurations.
We provide full design services, buyer label customization, and rapid turnaround for pilot tooling runs, enabling San Fernando developers to validate prototype drivetrains within weeks.
Rigorous Factory Acceptance Testing (FAT)
Every piece of equipment built in our Ningbo facility undergoes comprehensive pre-shipment trial runs using the customer's actual lamination samples, magnet grades, and magnet wire specifications.
We conduct transparent multi-angle video acceptance inspections and provide sample validation batches for micro-sectioning and surge testing before release, ensuring zero-risk international commissioning.
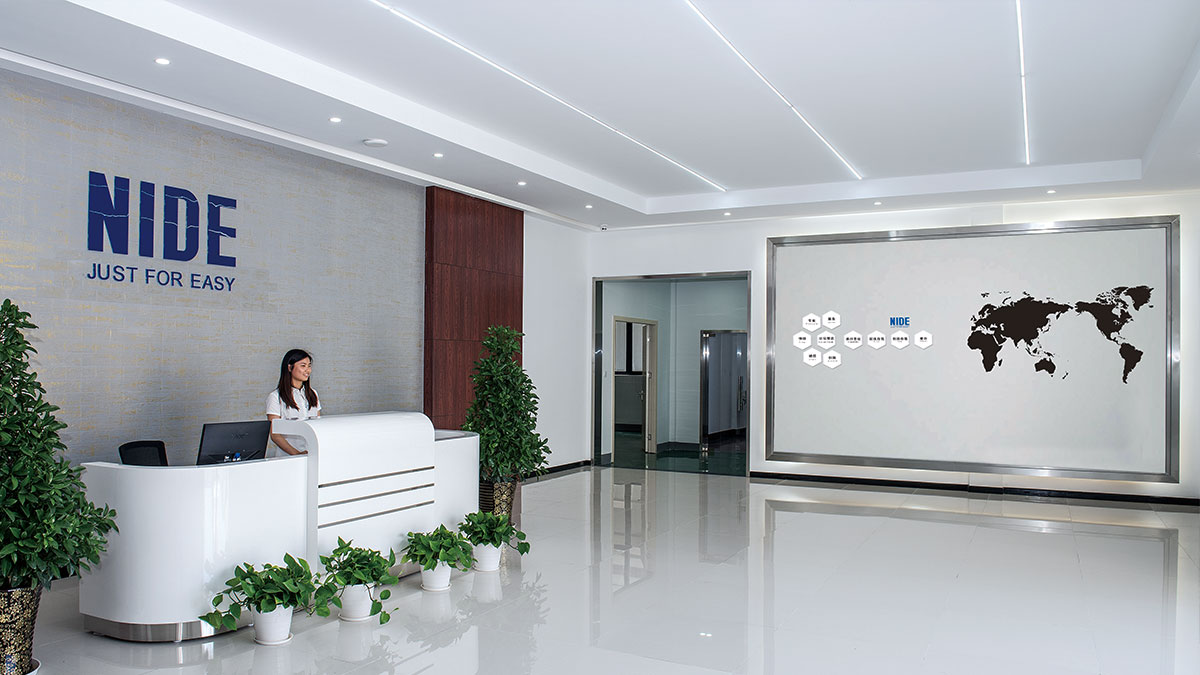
Modern Heavy Assembly Complex
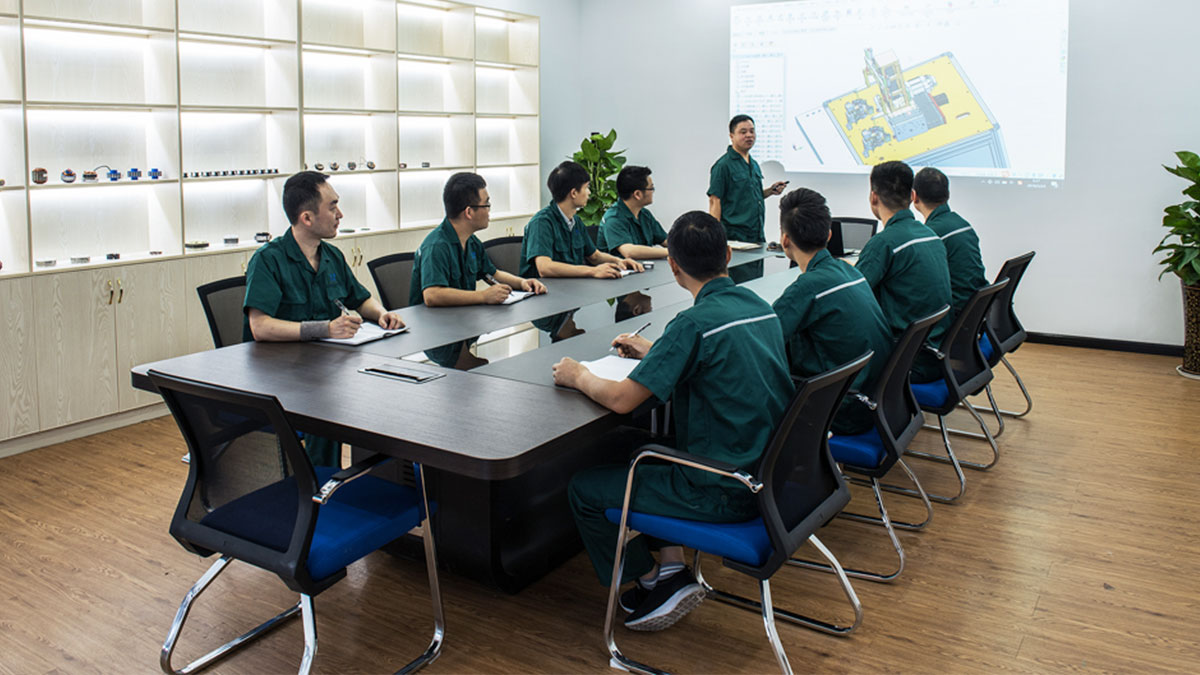
Precision Stator Machine Workshop
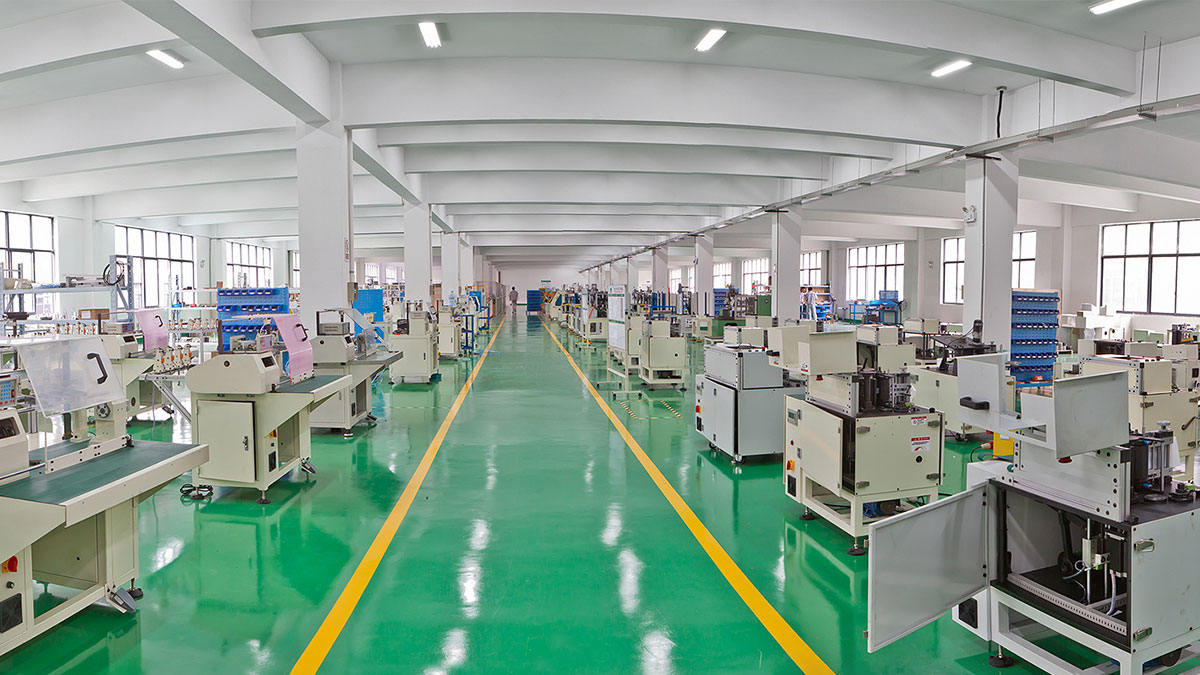
Factory Run-Off Verification
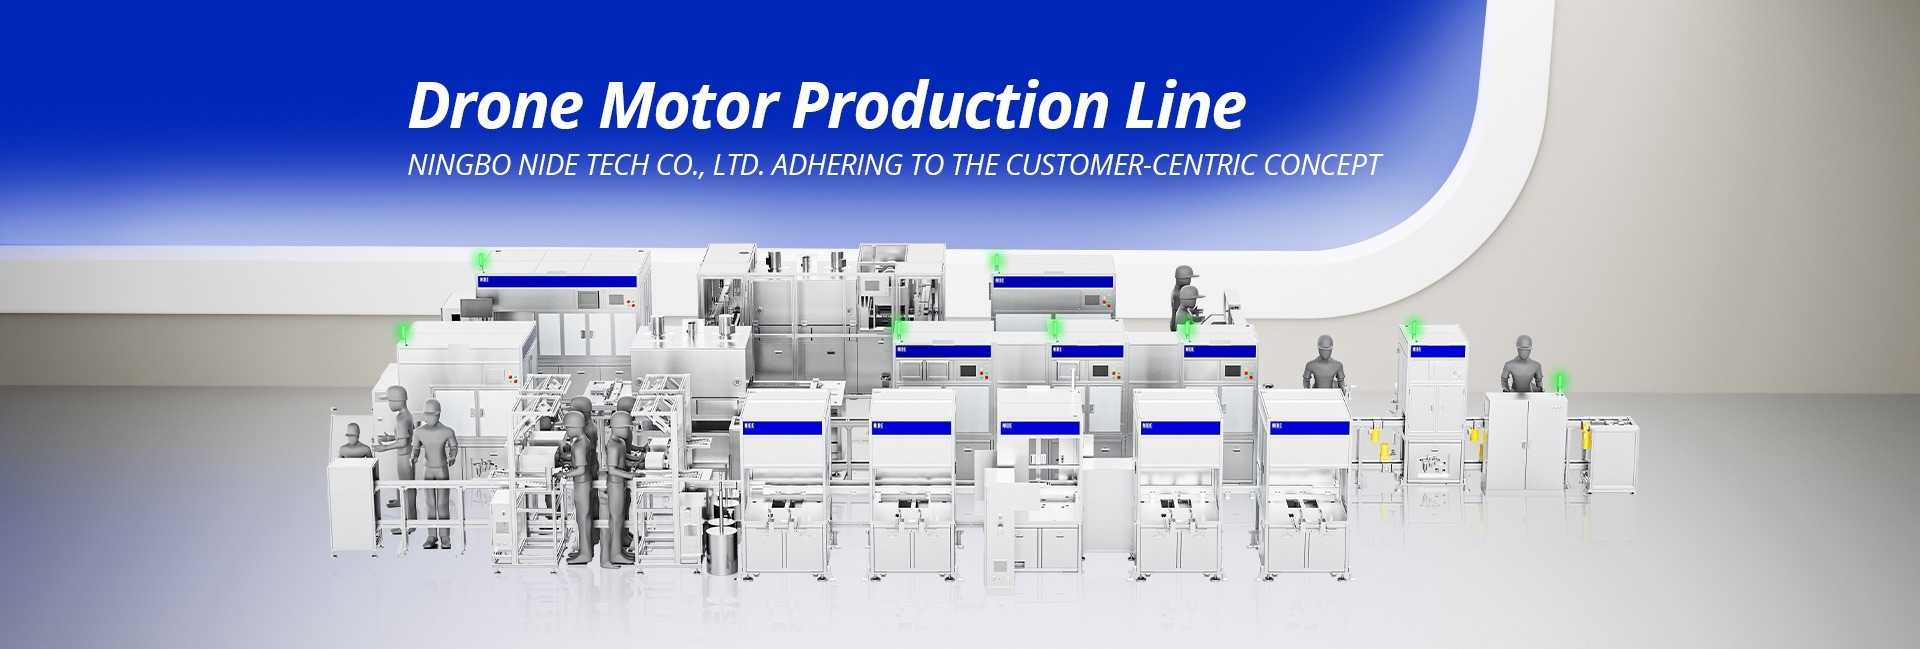
Turnkey Automated Production Cells
Procurement & Technical FAQ for San Fernando Buyers
Detailed guidance on import procedures, electrical utility compatibility, on-site commissioning, and regulatory certifications for California engineering procurement teams.
How do you manage freight logistics and shipping to San Fernando facilities?
Equipment destined for San Fernando buyers ships in heavy-duty, moisture-sealed, seaworthy wooden cases through the Port of Ningbo directly to the Port of Los Angeles (POLA) or Port of Long Beach (POLB). Ocean transit time is typically 14 to 18 days. From the harbor, our experienced freight forwarders coordinate customs clearance, bonded drayage, and flatbed delivery directly to your facility in San Fernando, Pacoima, Sylmar, or Burbank under DDP, CIF, or FOB trade terms.
Are machine electrical cabinets adapted for California industrial utility standards (480V / 208V, 60Hz)?
Yes. All electrical systems, power cabinets, servo drives, and induction frequency converters are engineered specifically to client specifications. For California plants, we configure the control architecture for 480V 3-phase 60Hz or 208V 3-phase 60Hz. We utilize UL-recognized industrial control components, including Schneider Electric or Siemens circuit breakers, Omron relays, and Mitsubishi or Siemens PLCs to ensure seamless local electrical inspection and OSHA compliance.
What level of on-site installation and field engineering training is provided in California?
We provide a hybrid support model. For turnkey lines, our senior field commissioning engineers travel to your San Fernando plant to oversee physical positioning, precision mechanical leveling, electrical tie-in, software integration, and pilot production run-offs. We offer bilingual English technical manuals, complete circuit diagrams, ladder logic source files, and conduct on-site operator and maintenance training. Furthermore, our machines feature secure VPN gateways for instant remote factory diagnosis.
Can your mid-drive motor lines assemble multiple motor models on the same line?
Yes. Modern motor production demands flexibility. Our assembly lines are designed around quick-change modular tooling. Stator coil winding nozzles, inserting tooling plates, and rotor balancing collets can be swapped out in under 25 minutes. Programmable recipe managers within the HMI touchscreen allow operators to switch parameters (wire turn counts, stack length offsets, torque limits, test profiles) with a single click.
How does Nakro ensure compliance with California UL 2849 safety certification requirements?
Compliance begins with process control. Our end-of-line testing rigs evaluate stator insulation resistance, inter-winding surge degradation, thermal rise under load, and dielectric breakdown up to 3,000V. By integrating automated torque testing, phase current balance verification, and back-EMF harmonics analysis, every motor leaving your line has a digital test certificate verifying conformity to UL 2849, CE, and ISO standards.
What is the standard manufacturing lead time and payment terms?
Standard stand-alone machines (such as single-operator coil winding or magnet inserting units) have an engineering build cycle of 45 to 60 days. Fully automated turnkey mid-drive stator and rotor production lines typically require 90 to 120 days from final drawing approval to Factory Acceptance Testing (FAT). Standard payment terms are 30% T/T advance deposit, 60% upon video trial run approval, and 10% against Bill of Lading, or irrevocable Letters of Credit (L/C).
Accelerate Your Powertrain Production in San Fernando
Send our senior engineering team your mid-drive motor 2D/3D CAD drawings, slot specifications, target output capacity, and factory floor dimensions. We will engineer a custom turnkey proposal, cycle time analysis, and layout within 48 business hours.
Contact Us