Featured Automated Machinery & Core Motor Components
Explore our field-tested automated equipment engineered specifically for high-efficiency rotor lines, armature coil winding, hot chamber die-casting, and high-conductivity commutating subsystems.

Automatic PLC Controlled BLDC Motor Rotor Magnet Inserting Machine
- Fully Automated Servo Indexing
- Precise Dispensing & Press-Fit
- Industrial 1-Year Core Warranty

New Automatic BLDC Armature Coil Winding Machine for Wheel Motor Stator
- High-Speed Multi-Flyer Winding
- CE Certified Core Components
- Integrated Electronic Tensioner

New Automatic Armature Rotor Hot Chamber Die Casting Machine
- Automated Aluminum Injection
- Siemens PLC Control Unit
- High Pressure Core Degassing

New Condition Planar Type Commutator Motor Component (NDPJ-HXQ-39)
- High Thermal Stability Phenolic
- Anti-Oxidation Copper Bar Face
- Certified for DC Automotive Pumps

Customized Commutator Armature with Copper Collector Hook
- Model NDPJ-HXQ-871A Spec
- Reinforced Hook Pull Strength
- Zero-Defect Tangent Fusion

NDPJ-TS-1 Automobile Electrical Carbon Brush Assembly
- Low Friction Electro-Graphite
- Exceptional Current Conductivity
- Ultra-Long Operational Lifetime

High Precision Motor Carbon Brushes for Small Electric Motors (NDPJ-TS-9)
- CE Certified Precision Metallurgy
- Minimal Sparking & Arc Suppression
- Optimized for Compact Drives

Automatic EV New Energy Motor Hairpin Stator & Rotor Line
- Complete 220V/380V Configuration
- Robotic Hairpin Laser Welding
- Industry 4.0 MES Traceability
Rotor Manufacturing Automation: Engineering Principles, Kinematics, and Quality Assurance
An in-depth analysis of dimensional tolerance control, magnetic flux optimization, structural integrity, and dynamic balancing criteria for contemporary electromechanical systems.
In modern electromechanical apparatus, the rotor assembly is the principal kinetic node dictating dynamic torque conversion, operating efficiency, electromagnetic noise signature, and machine lifespan. Whether manufacturing squirrel-cage induction rotors, brushless permanent magnet (BLDC/PMSM) rotors, or wound universal armatures, precision engineering must reconcile conflicting mechanical stresses, thermal dilation rates, and high-frequency magnetic reversals. As a premier rotor assembly line supplier and exporter in Peja, our system architectures are built to exceed strict European standards (EN 60034 series), guaranteeing that industrial enterprises across Kosovo and the Balkan trade routes achieve cycle times under 15 seconds per unit while maintaining micron-scale shaft runout tolerances.
Lamination Stacking & Pressure Skewing
Precision servo-hydraulic press systems compact high-permeability silicon steel stampings (0.35mm–0.50mm thickness) with controlled axial force. Automated angle-skewing modules mitigate slot harmonics, cogging torque, and mechanical vibration, establishing consistent magnetic flux density along the rotor core package.
High-Pressure Aluminum Hot Die-Casting
For asynchronous induction motors, our automated hot chamber die-casting cells deliver molten pure aluminum (or copper-aluminum alloy) directly into the rotor slot channels under controlled chamber pressure, eliminating internal porosity, blowholes, and uneven end-ring resistance profiles.
Automated Magnet Insertion & Gluing
Permanent magnet BLDC rotors require meticulous polarity-checked insertion. Our machines integrate vision-guided positioning, dual-component anaerobic adhesive dispensing, and heat-induction curing stations to lock NdFeB/Ferrite permanent magnets securely against centrifugal forces exceeding 20,000 RPM.
A critical phase in our automated sequence is two-plane dynamic balancing, which isolates both static and dynamic unbalance moments using high-sensitivity piezoelectric force transducers. Imbalance compensation is carried out automatically via multi-axis CNC milling cutters or precision axial drilling heads, eliminating manual weights and ensuring operational balance quality classes conforming strictly to ISO 1940-1 Grade G2.5 or G1.0.
| Performance Specification | Universal Armature Rotor Line | BLDC / PMSM Motor Rotor Line | Induction Squirrel-Cage Line |
|---|---|---|---|
| Target Core Diameter Range | Ø18 mm – Ø75 mm | Ø20 mm – Ø140 mm | Ø40 mm – Ø260 mm |
| Maximum Core Stack Height | Up to 120 mm | Up to 220 mm | Up to 350 mm |
| Production Cycle Time (Takt) | 8.0 – 14.0 seconds / pc | 12.0 – 22.0 seconds / pc | 18.0 – 35.0 seconds / pc |
| Shaft Runout Precision (T.I.R.) | ≤ 0.003 mm | ≤ 0.002 mm | ≤ 0.005 mm |
| Residual Dynamic Unbalance | ≤ 0.5 mg·mm (ISO G1.0) | ≤ 0.3 mg·mm (ISO G1.0) | ≤ 1.0 mg·mm (ISO G2.5) |
| Control Architecture & Fieldbus | Siemens S7-1500 / Profinet | Mitsubishi iQ-R / EtherCAT | Omron Sysmac / Profinet |
Localized Application Scenarios in Peja & Kosovo Manufacturing Hubs
How advanced rotor production lines empower Peja's growing mechanical processing, renewable engineering, beverage bottling automation, and electric mobility infrastructure.
The city of Peja (Peć), situated strategically in western Kosovo at the foot of the Accursed Mountains along the Bistrica river, has established itself as an economic hub known for robust beverage bottling facilities, wood processing, light metallurgical engineering, and agricultural equipment fabrication. As Kosovo continues its proactive industrial modernization and EU harmonization, manufacturing entities in Peja, Pristina, Gjakova, and Ferizaj face mounting demand for localized electric drive assembly to displace imported sub-assemblies and capture regional supply chain value.
Beverage & Agro-Processing Drives
Peja's commercial breweries, food-grade packaging facilities, and automated dairy plants require dependable three-phase induction and wash-down stainless motors. Our rotor lines assemble sealed, vibration-resistant rotors that guarantee long-life cycle operation under continuous hygienic duty cycles.
HVAC & Ventilation Systems
With rigorous energy efficiency mandates throughout Kosovo and surrounding Balkan territories, HVAC manufacturers in Peja are transitioning from shaded-pole motors to electronically commutated (EC) BLDC rotors, achieving up to 35% reduction in commercial electrical consumption.
Light E-Mobility & Delivery Fleets
Urban logistics in Peja, Prizren, and Pristina are embracing electric two-wheelers, light delivery tricycles, and municipal vehicles. Our automated wheel hub motor and outer-rotor assembly machinery produce high-torque, durable permanent-magnet brushless propulsion hubs locally.
Hydraulic & Deep-Well Water Pumps
Extensive agricultural irrigation across the Dukagjini valley calls for reliable submersible pump motors. Our rotor lines feature anti-corrosion shaft knurling, precision copper bar brazing, and epoxy encapsulation to prevent water ingression and premature rotor burnout.
By establishing localized rotor assembly operations in Peja, domestic manufacturers achieve strategic insulation against global maritime logistical disruptions, reduce warehousing footprint via Just-In-Time (JIT) batch scheduling, and leverage Kosovo’s competitive labor base and zero-tariff trade frameworks across CEFTA member nations.
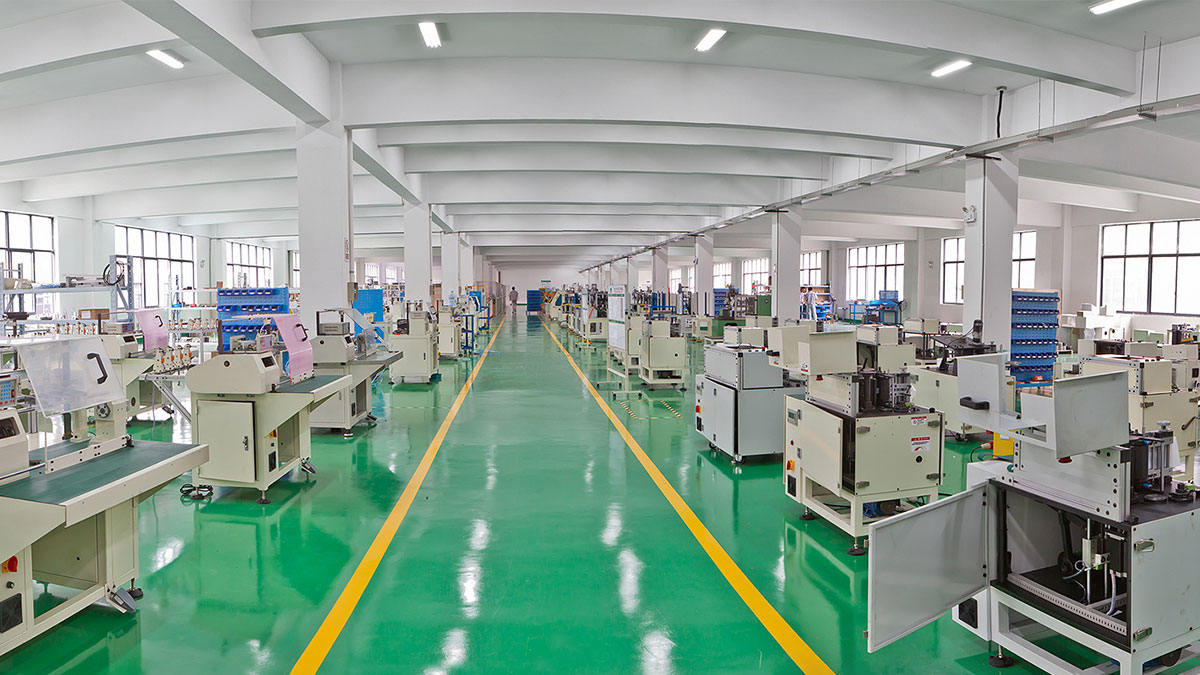
Inside Our Machine Tooling & Assembly Workshops
Over 30,000 m² of modern CNC machining centers, trial-run platforms, and robotic test cells delivering proven manufacturing reliability since 2010.
Industrial Evolution: Emerging Rotor & Electromobility Trends in Western Kosovo
Analyzing economic catalysts, CEFTA export dynamics, nearshoring imperatives, and European Green Deal initiatives shaping regional manufacturing investments.
The industrial landscape in Peja and the Western Balkans is experiencing a profound pivot driven by four macroeconomic forces: the pan-European nearshoring movement, the EU Carbon Border Adjustment Mechanism (CBAM), rising logistics tariffs from East Asia, and targeted domestic capital incentives for clean-tech industrialization. For electro-mechanical engineering enterprises situated along the R107 and M9 transit arteries connecting Peja to Albania and Montenegro, integrating modular rotor production equipment provides distinct operational leverage:
Nearshoring to European OEMs
European motor integrators are actively seeking component tier-suppliers within a 48-hour road haul. Located near the Port of Durrës and Mediterranean corridors, plants in Peja equipped with our automated rotor lines can export finished, high-precision armatures and rotors directly into Germany, Austria, and Italy without costly sea-freight delays.
IE3 to IE5 Efficiency Directives
Kosovo's ongoing energy efficiency reforms are aligning regional industrial standards with European Commission Ecodesign regulations. High-efficiency synchronous reluctance rotors and permanent magnet rotors assembled on our lines drastically minimize electrical losses, directly meeting stringent IE4 and IE5 efficiency thresholds.
Data-Driven Smart Production (MES)
Local enterprises are leaving behind manual workshops in favor of Industry 4.0 automation. Our rotor lines feature Ethernet/IP and OPC-UA connectivity, barcode-tracked torque records, dimensional laser scanning, and remote cloud diagnosis, guaranteeing full end-to-end traceability for every rotor shipped.
Enterprise Competence & Engineering Differentiators
As a dedicated equipment designer and manufacturer established in 2010, Ningbo Nakro Intelligent Equipment delivers turnkey reliability, comprehensive tooling support, and global field engineering.
Selecting a capital equipment partner requires transparent engineering capability, rigorous quality management, and dedicated lifecycle assistance. Ningbo Nakro Intelligent Equipment Co., Ltd. operates state-of-the-art facilities covering over 30,000 square meters in Ningbo, China, backed by more than 13 years of specialized machinery export experience across over 50 countries in Europe, the Americas, the Middle East, and Southeast Asia. Our advantage lies in complete vertical integration: we do not merely supply machines—we deliver total process security from initial motor component drawing to steady-state serial production.
ISO 9001 & CE Certified
Every rotor machine, electrical cabinet, and safety enclosure complies fully with European Machinery Directives, equipped with Pilz safety relays, CE-certified pneumatics, and robust protective shielding.
Bespoke Tooling & Quick-Change
Our engineering department custom designs high-grade SKD11/tungsten carbide inserting blades, winding heads, and collets. Tooling changeovers can be executed in under 20 minutes for high-mix agility.
One-Stop Subcomponent Access
Beyond machinery, we supply the complete matching component ecosystem—precision planar commutators, collector hooks, carbon brushes, high-speed ball bearings, balance clips, and insulation films.
Dedicated Western Balkan Support
Through remote diagnostic gateways and experienced regional service partners, we provide on-site commissioning, electrical training, routine preventive maintenance schedules, and rapid spare parts replenishment.
Five-Stage Engineering & Delivery Workflow
Our standardized project methodology eliminates operational risk from initial motor drawing evaluation to final factory sign-off.
Drawing Analysis
Thorough evaluation of rotor laminations, shaft tolerances, slot configurations, and annual production volumes.
System Proposal
Custom 3D line layout modeling, cycle time simulations, station automation levels, and formal budget quotation.
Manufacturing & FAT
Precision fabrication, assembly, and rigorous Factory Acceptance Testing (FAT) using client-supplied raw materials.
Logistics & Delivery
Seaworthy anti-corrosion packaging, maritime transport to Adriatic ports, customs assistance, and inland transit to Peja.
On-Site Commissioning
Mechanical installation, electrical fine-tuning, operational staff training, and full production hand-over.
Six-Tier Quality Control Protocol Before Dispatch
Every machine tool leaving our facility is certified under stringent multi-point metrological and electrical stress tests.
Raw Material & Metallurgy
Spectrometric and ultrasonic testing of all structural tool steels, casting frames, pneumatic valves, and servo actuators against ISO and DIN criteria.
Micro-Tolerance Machining
Precision coordinate-measuring machine (CMM) inspection of custom insertion mandrels, winding flyers, and guide tooling to ensure sub-5µm accuracy.
Control Logic & Safety Audit
Validation of PLC software subroutines, electrical interlocking, emergency stop responses, and HMI alarm diagnostics under simulated fault modes.
Continuous Run-Off (FAT)
48-hour continuous simulated cycling using actual customer rotor shafts, laminations, and magnets to verify thermal stability and takt time consistency.
Finished Part Metrology
Complete runout, magnetic flux dispersion, dielectric resistance, and residual dynamic unbalance testing of trial-run rotors produced on the line.
Maritime Export Packaging
Vacuum moisture barrier wrapping, vapor corrosion inhibitor (VCI) application, shock indicators, and reinforced solid-fumigated timber crate packing.
Frequently Asked Questions for Peja & Regional Industrial Buyers
Clear, expert responses to technical integration, shipping logistics, customs documentation, electrical compatibility, and maintenance protocols.
What rotor motor types can your assembly lines accommodate in a Peja production facility? +
How are machines delivered to Peja, Kosovo, and what are the standard shipping transit times? +
Are Nakro rotor assembly lines fully compatible with Kosovo’s electrical grid specifications? +
Can you assist our Peja engineering team with factory line layout, cycle-time modeling, and tooling? +
What level of on-site installation, commissioning, and operator training is provided in Kosovo? +
What commercial payment terms, currency options, and warranty packages do you accept? +
Plan Your Rotor Production Line Upgrade in Peja Today
Whether you are establishing a new electromechanical manufacturing plant, automating existing manual workstations, or expanding high-efficiency motor production in Kosovo, our engineering team is ready to analyze your drawings and propose a bespoke, high-efficiency turnkey solution.
