Standardized & Tailored Welding Line Equipment
Explore our flagship automated fusing machinery, rotor assembly stations, hook commutators, and precision magnetic components configured to withstand demanding sub-alpine operating profiles.

Rectangular N52 NdFeB Neodymium Magnets Model NDPJ-CW-58
Ultra-high remanence sintered rare-earth magnets engineered for micro-motor flux consistency and peak torque stabilization in alpine ventilation systems.

Copper Hook Commutator Armature Model NDPJ-HXQ-871A
0.05% Silver-alloyed copper collector segment armature with precision hot-fusing tangs configured for low resistance and minimal runout.

Radiator Cooling Fan Motor Armature Hook Commutator
Universal automotive cooling commutator featuring thermal fatigue-resistant copper profiles adapted to severe thermal switching cycles.

Automobile Carbon Brush Parts Model NDPJ-TS-1
Optimized electro-graphite compositions designed to provide uniform film formation and suppress commutation spark discharge.
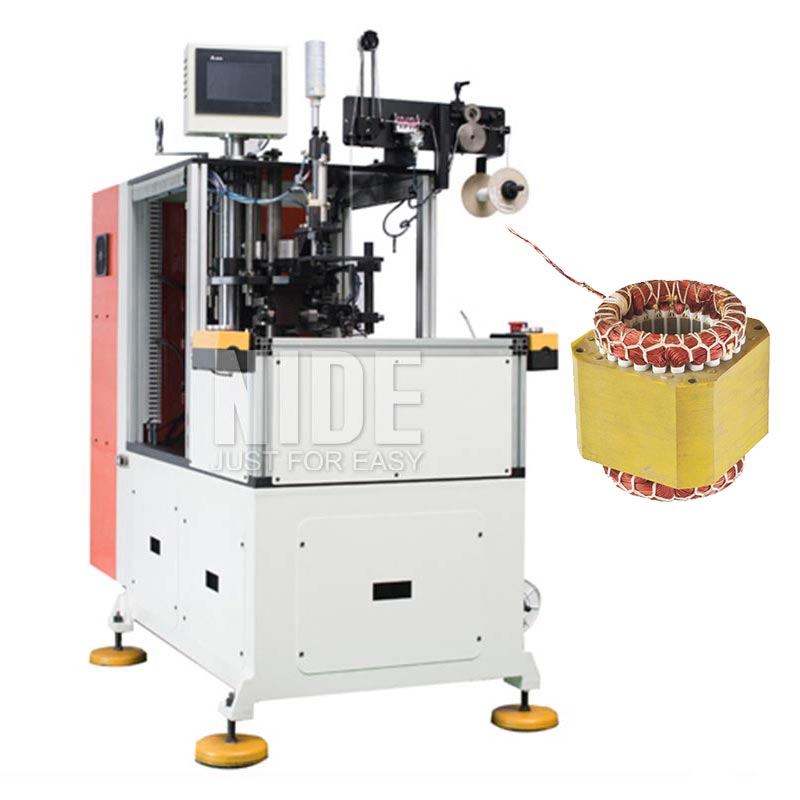
Automatic Double Ends Stator Coil Lacing Machine
PLC-synchronized dual-end stator binder delivering 10kW servo binding performance for severe environmental hydro and HVAC motors.

Juicer Mixer DC Motor Armature Model NDPJ-HXQ-183
High-speed balance rotor with cold-forged commutating segments designed for precision consumer appliances and hospitality kitchen units.

24 Segments Hook Type Angle Grinder Commutator
Heavy-duty 8.4*25*16 commutator tailored for high-vibration power tools, industrial grinders, and continuous maintenance machinery.

Automatic Single Phase Motor Stator Coil Inserter
CE-certified high-speed simultaneous wedge inserting and coil loading unit engineered to avoid wire scrape on premium enamel coatings.
Micro-Resistance Fusing vs. TIG/Laser Commutator Bonding
Evaluating structural metallurgy, intermetallic phase stability, and thermal stress mitigations during automated armature hot stacking.
Thermal Dissipation & Enamel Burn-off Dynamics
In modern universal, fractional horsepower, and automotive DC motor manufacturing, commutator welding represents the single most thermally sensitive junction. Motor commutator welding equipment (commonly known as hot stacking or resistance commutator welders) must achieve two distinct physical transformations in a single, precisely governed cycle: instantaneous thermal stripping of the polyurethane or polyamide-imide wire insulation varnish, followed immediately by solid-state diffusion bonding or micro-resistance fusing between the oxygen-free copper wire and the commutator tang (hook or slot segment).
The engineering challenge lies in energy metering. If heat transfer exceeds 350 Joules per millisecond, thermal migration down the copper segment causes resin degradation in the commutator molding compound (phenolic or polyphenylene sulfide), yielding mica dislocation, high-bar faults, and peripheral runout. Conversely, inadequate energy delivers cold joints, leaving unvaporized polymer residues that elevate electrical contact resistance above allowable thresholds (typically <0.5 milliohms per hook). Our intelligent inverter DC fusing power sources utilize closed-loop displacement monitoring: the electrode applies a controlled pre-squeeze force, delivers an upslope pulse that burns the enamel clean, adjusts downward displacement in real time (within ±0.01 mm), and delivers the forging current pulse that collapses the hook into an airtight, intermetallic bond.
Constant Inverter Current
4kHz/8kHz medium-frequency inverter DC systems minimize magnetic losses and deliver microsecond response rates, preventing current surges that blow hook tips.
Dynamic Displacement Control
Linear variable differential transformers (LVDT) gauge hook collapse height in real-time, halting discharge when exact mechanical deformation is attained.
Pneumatic-Servo Pressure Heads
Dual-stage force profiling isolates pre-welding clamping from follow-up forging force, eliminating electrode bouncing and arc spatter across segments.
Multi-Index Rotor Fixturing
Harmonic servo indexing drives index copper commutators up to 36 slots in under 4 seconds, maintaining circumferential runout tolerance below 0.003 mm.
Engineered by Nakro: Global Reach, Precision Control
Ningbo Nakro Intelligent Equipment Co., Ltd. integrates automated coil winding, commutator joining, and full-line testing architectures backed by deep industrial manufacturing roots.
Why Leading Motor Manufacturers Partner With Our Plants
Ningbo Nakro Intelligent Equipment operates between 30,000 and 50,000 square meters of specialized mechanical assembly workshops, CNC tooling facilities, and clean electrical testing centers. Our technical team comprises over 100 dedicated automation engineers, machine designers, and quality specialists whose machinery generates an annual export turnover between US$10M and US$50M. We do not merely assemble frames; we engineer turnkey value chains—supplying every component from high-grade commutators, custom copper hooks, NdFeB permanent magnets, and carbon brushes to automated lacing and coil insertion machines.
Every piece of motor commutator welding equipment leaving our bays undergoes six rigid QC checkpoints: raw mechanical hardness verification, precision EDM tungsten-electrode profiling, high-voltage electrical cabinet burn-in, trial runs using our clients' actual wire and commutators, weld shear tests, and seaworthy nitrogen-purged moisture encapsulation. Backed by verified Alibaba Onsite inspections, third-party audit credentials, and multi-currency settlement structures (USD, EUR, CNY), we provide full technical security for industrial enterprises in Europe and across the globe.
Localized Application Scenarios in Escaldes-Engordany
Addressing the rigorous mechanical stresses imposed by thermal swings, elevation, and premium hospitality infrastructure in the parish of Escaldes-Engordany, Andorra.
Thermal Spring Pumping & Balneotherapy
Escaldes-Engordany is renowned worldwide for its sulfur-rich thermal waters and balneotherapy complexes such as Caldea. Circulating high-temperature, mineral-dense water demands fractional DC and permanent-magnet booster pumps wound with zero voids. Resistance welding ensures the hook junctions never delaminate under 24/7 continuous duty cycles in elevated ambient steam conditions.
Sub-Alpine EV & E-Mobility Powertrains
Navigating high-altitude Pyrenean inclines and cold-weather descent regenerations puts severe cyclic amperage spikes through traction and auxiliary motor armatures. Hot stacking eliminates micro-arcing between segment hooks, guaranteeing zero thermal failure for light electric delivery trikes, scooters, and utility ski-maintenance vehicles.
HVAC & Clean Hydroelectric Generation
Modern commercial infrastructure and high-efficiency mountain hydro stations throughout the Valira d'Orient river basin require automated, repeatable stator inserting and commutator welding to preserve high electrical efficiency factors, reducing operational grid load during peak winter tourism seasons.
Electromechanical Trends in Andorra & Escaldes-Engordany
How regional decarbonization, building automation, and high-altitude electrification shape procurement requirements for electric motor manufacturing assets.
Low-Noise Building Automation Standards
Luxury hospitality resorts, commercial hubs, and wellness centers in Escaldes-Engordany enforce strict acoustic thresholds. Commutator runout generated by uncalibrated welding setups results in severe brush chatter and acoustic resonance. Modern automated fusing guarantees balanced rotors that meet European Class A noise restrictions.
Shift from Carbon to Brushless Transitions
While classic power tools and universal motors rely on hook commutators, local industrial engineering firms are progressively specifying hybrid BLDC manufacturing solutions. Nakro provides bridge machinery capable of servicing both universal armatures and BLDC needle-wound stators within the same facility footprint.
Predictive Quality Traceability (Industry 4.0)
Andorran maintenance workshops and electromechanical suppliers increasingly demand digitized weld signatures. Our equipment records peak amperage, electrode displacement, and thermal curves per commutator hook, compiling CSV quality dossiers for immediate compliance validation.
Frequently Asked Questions for Regional Procurement
Clear technical, operational, and shipping answers for mechanical workshops, utilities, and line managers in Escaldes-Engordany and surrounding European territories.
What are the key technical differences between hot stacking and TIG welding for commutators?
+
How do you handle shipping, customs clearance, and delivery to Escaldes-Engordany?
+
Can your commutator welding machines handle dual or heavy parallel-wound magnet wires?
+
What power configuration and facility connections are needed in our workshop?
+
How is pre-shipment trial run and acceptance validation conducted?
+
What after-sales service and spare parts availability exist for European installations?
+
Elevate Your Rotor Commutator Joining Precision
Consult with our process engineers today. Send your rotor drawings, commutator hook dimensions, and line throughput goals for a comprehensive tooling specification and competitive quote.
