Featured Stator Assembly & Electromagnetic Subsystem Hardware
Direct from Ningbo Nakro Intelligent Equipment: Industrial-grade automated assembly lines, precision commutators, rare-earth magnets, and core winding components serving Finnish engineering manufacturers.








Industrial Stator Automation in Southwest Finland: Maritime Electrification & Cleantech Drives
An analytical overview of automated stator production line deployment for mechanical engineering firms, electrical machine builders, and system integrators operating within the Turku economic zone.
Marine & Port Electrification
Turku is the historic nucleus of Finnish shipbuilding, host to the renowned Meyer Turku shipyard and an expansive ecosystem of naval architects, electric propulsion specialists, and crane drive fabricators. The local industrial transition toward zero-emission Baltic vessels, electric harbor tugs, hybrid workboats, and automated shore-power winches has created an urgent demand for high-reliability permanent magnet synchronous motor (PMSM) and asynchronous induction stators capable of sustaining high salt-mist and high-vibration maritime duty cycles.
High-Efficiency Cleantech Powertrains
Across Southwest Finland (Varsinais-Suomi), stringent EU Ecodesign directives (Regulation EU 2019/1781) dictate minimum efficiency classes of IE3, IE4, and emerging IE5 Super Premium levels. Meeting these standards requires high-slot-fill copper winding lines where automated needle winders, CNC coil inserting machines, and precision 3D end-turn forming cells minimize active copper mass, eliminate turn cross-overs, and reduce total harmonic distortion (THD) and core excitation losses.
Arctic-Grade Thermal & Mechanical Rigor
Electric machinery deployed in Nordic heavy industry, offshore aquaculture, subsea pumping, and Finnish forestry processing requires advanced slot insulation insertion, dual-filament lacing, and automated trickle-resin or vacuum pressure impregnation (VPI) compatibility. Stator cores processed on Nakro equipment exhibit superior resistance to thermal shock, slot breakdown, and partial discharge phenomena down to -40°C ambient operating profiles.
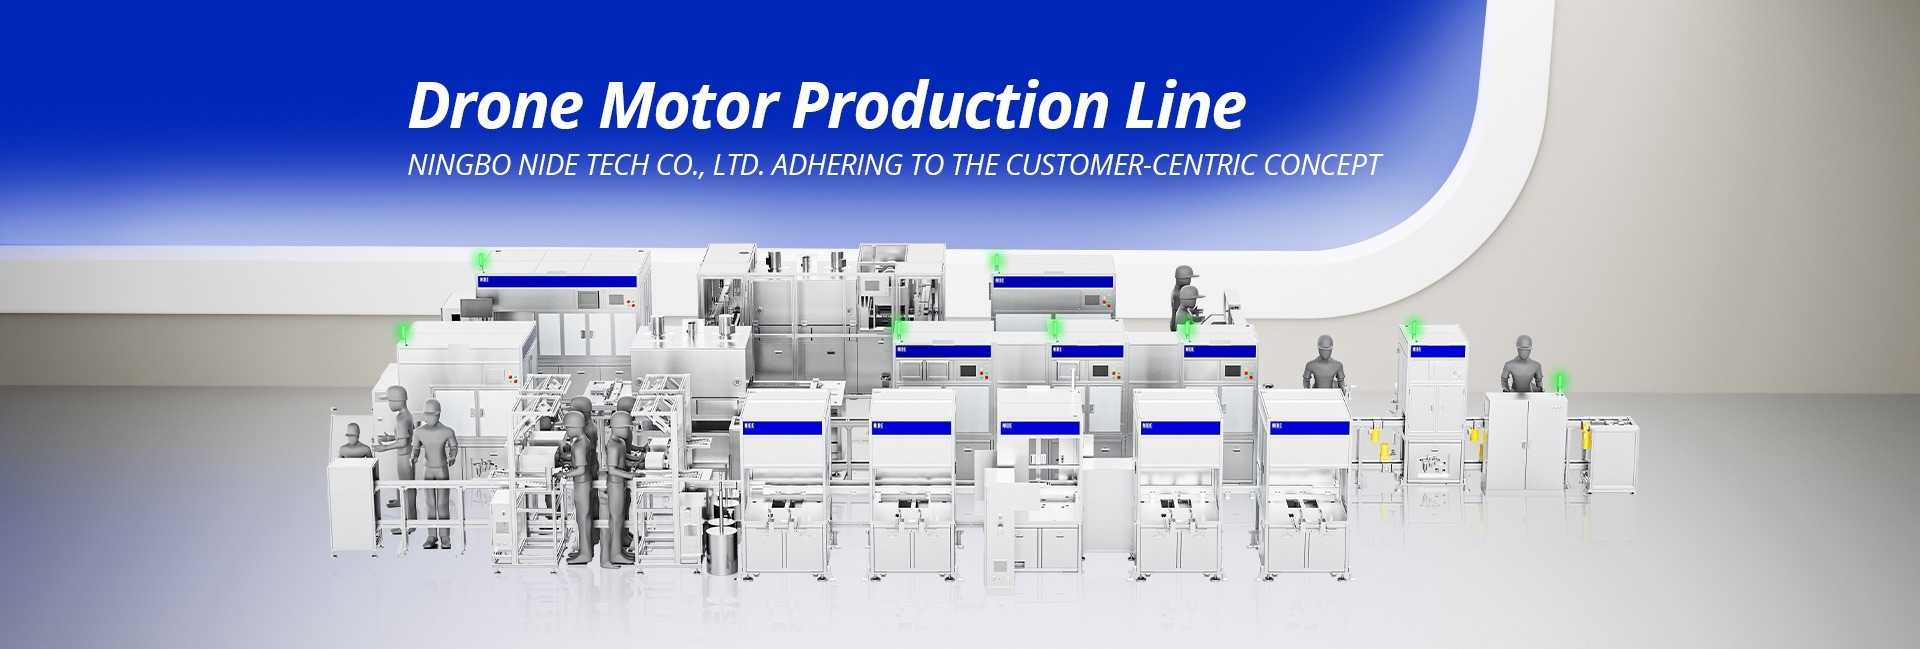
Full Automated Stator Assembly Line: Stage-by-Stage Breakdown
From raw lamination stacks to certified, tested wound stators: How Ningbo Nakro Intelligent Equipment delivers a complete Industry 4.0 turnkey workflow compliant with European safety norms.
CNC Slot Insulation Insertion
Automatic feeding, edge-creasing, cutting, and insertion of Nomex, DMD, or Kapton composite insulation paper into stator slots. Servo indexing ensures accurate cuffing at both laminate faces, preventing conductor abrasion during wire entry.
Coil Winding & High-Speed Transfer
Multi-spindle flyer or needle winding stations wind enameled copper or hairpins directly or via transfer tooling. Closed-loop magnetic brake tensioners preserve enamel dielectric integrity across fine to heavy round copper profiles.
Synchronous Coil & Wedge Insertion
Simultaneous push-rod actuation drives pre-wound coil bundles and epoxy/fiberglass wedges into the stator bore. Wedge feeding from continuous strip with automatic cutoff guarantees zero mechanical overhang beyond core tolerances.
Intermediate Stator End-Turn Forming
Progressive hydraulic or mechanical press forming flattens and flares the stator winding overhangs. Clears internal bore clearance for subsequent rotor clearance and creates pathways for phase insulation sheets.
Automatic Dual-End Coil Lacing
Double-needle servo CNC lacing mechanisms bind both upper and lower coil overhangs with high-tensile polyester tape or fiberglass cord. Programmable stitch pitches accommodate jumper leads and internal thermal sensors.
Final Hydraulic 3D Sizing
Expanding internal mandrel combined with segmented outer clamps compresses the coil overhangs to exact CAD drawing envelopes, guaranteeing hassle-free installation into cast-iron or aluminum motor enclosures.
End-of-Line (EOL) Electrical Testing
Automated pneumatic fixture clamps the stator leads to execute an automated multi-parameter test sequence: DC winding resistance, Insulation Resistance (IR > 100MΩ at 1000V), AC Hipot (2.5kV to 5kV), and Surge Waveform comparison.
Traceability & MES Data Logging
Laser etching of QR/DataMatrix codes on the lamination core linked with real-time test parameters, cycle time, insertion forces, and wire batch data via OPC UA for Finnish factory MES and ERP integrations.
| Station / Parameter | Standard Induction Motor Line | BLDC / PMSM Stator Assembly Line | Marine Propulsion / Heavy EV Stator Cell |
|---|---|---|---|
| Stator Outer Diameter (Ø) | 40 mm – 260 mm | 18 mm – 180 mm | 120 mm – 450+ mm |
| Lamination Stack Height | 15 mm – 300 mm | 10 mm – 200 mm | 50 mm – 500 mm |
| Applicable Wire Diameters | Ø 0.18 mm – 1.40 mm (Round) | Ø 0.12 mm – 1.60 mm (Single/Multi-strand) | Heavy round up to 2.2 mm or Hairpin flat wire |
| Winding Technology | Flyer / Tooling transfer + Inserter | CNC Multi-axis Needle Winding | Dual-needle direct tooth or Hairpin bending |
| Control Architecture | Siemens S7-1500 / Omron Sysmac PLC | Beckhoff TwinCAT / Siemens Motion PLC | Siemens TIA Portal with Safety Integrated |
| CE Directives Compliant | 2006/42/EC, 2014/35/EU, 2014/30/EU | 2006/42/EC, 2014/35/EU, 2014/30/EU | 2006/42/EC, 2014/35/EU, EN ISO 13849-1 Cat 4 |
Key Strategic Trends Driving Stator Sourcing in Turku
Why precision automation, local compliance, and component agility represent a competitive edge for Finnish manufacturers facing global supply chain challenges.
Reshoring & Nearshoring of Core Powertrains
Nordic machine builders are mitigating single-source overseas sub-assembly risks by repatriating motor manufacturing capabilities. Investing in a flexible Nakro stator winding and inserting line allows Turku-based OEMs to produce customized lot sizes on demand, slashing transit lead times from weeks to hours and protecting intellectual property around proprietary magnetic slot geometries.
Stringent CE Safety & Finnish Safety Standards (TUKES)
Machinery installed in Finland must undergo rigorous verification under the Finnish Safety and Chemicals Agency (TUKES) framework in alignment with the EU Machinery Directive. Nakro equipment features Category 4 / PL e safety light curtains, interlocked aluminum access enclosures, emergency stop loops, and isolated low-voltage control cabinets that fully satisfy Finnish workplace occupational safety auditors.
Harmonized Component & Machine Sourcing
Unlike conventional machine brokers who supply only bare mechanisms, Nakro leverages a comprehensive dual-competency model: providing fully commissioned stator machinery alongside matched mechanical and electrical consumables (high-grade N52 neodymium magnets, permanent ferrite arc segments, copper commutators, and carbon brushes). This eliminates interface mismatch and ensures unified engineering accountability.
About Ningbo Nakro Intelligent Equipment Co., Ltd.
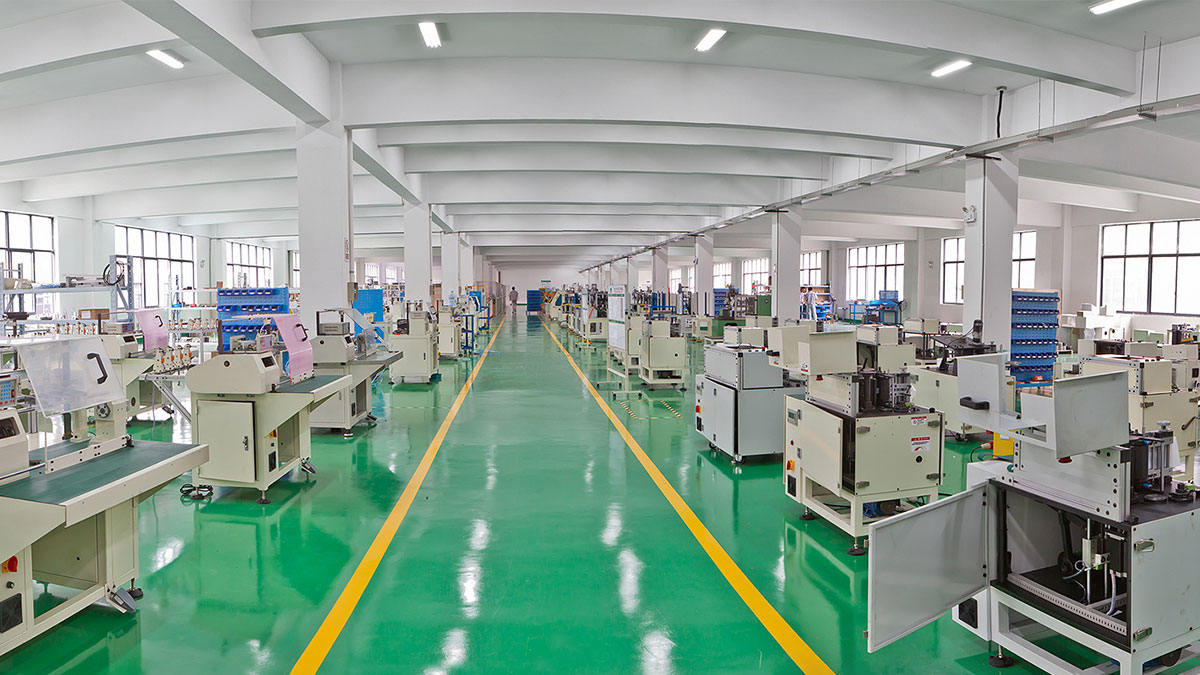
Established in 2010, Nakro has developed into an internationally certified powerhouse in electric motor manufacturing technology, operating modern facilities exceeding 30,000 square meters.
Turnkey Engineering Depth
Nakro engineers maintain complete mastery over the motor manufacturing lifecycle. Our core R&D team designs proprietary winding nozzles, hardened tungsten insertion blades, multi-wire flyer flyers, and servo-actuated forming dies engineered specifically around client-provided CAD lamination geometries.
Rigorous Pre-Shipment Run-Off (FAT)
Every stator winding machine and integrated production line undergoes an exhaustive Factory Acceptance Test (FAT) prior to crating. Buyers supply sample laminations, copper magnet wire, and phase insulation, allowing us to perform continuous trial production runs with full video documentation and electrical test reporting.
Global Commissioning & Spares
With machine exports reaching more than 50 industrial countries over 13+ years, Nakro maintains comprehensive international technical support networks. We provide remote real-time VPN telemetry diagnostics, on-site commissioning by experienced field technicians, and rapid express dispatch of wear tooling to Finland.
Turku Technical Procurement FAQ
Essential technical, compliance, and commercial guidance for Finnish engineering buyers evaluating stator production systems.
Q1: How does Nakro verify compliance with the European CE Machinery Directive for Finnish installations?
All Nakro stator production equipment shipped to the Turku market is manufactured under our ISO 9001 quality system and strictly adheres to CE Directive 2006/42/EC (Machinery), 2014/35/EU (Low Voltage Directive), and 2014/30/EU (Electromagnetic Compatibility). The electrical architecture follows EN 60204-1 safety standards, utilizing branded safety relays, dual-channel emergency stop circuits, IP54-rated enclosures, and certified safety interlocks. Complete Technical Construction Files (TCF) and official Declarations of Conformity (DoC) accompany every machine delivery.
Q2: Can the stator line adapt to multiple motor frame sizes and varying stack heights?
Yes. Nakro machines utilize quick-change tooling fixtures and modular recipe management within the PLC HMI. For instance, transitioning between IEC 80 and IEC 90 stator laminations requires less than 25 minutes of mechanical tool swapping (insertion tooling, wedge guides, and forming mandrels), followed by selecting the pre-saved digital recipe on the touchscreen to adjust stroke lengths, turn counts, and indexing angles.
Q3: Can Nakro handle high slot fill factors (>75%) required for IE4/IE5 high-efficiency stators?
Our multi-axis CNC coil inserting and forming stations are specifically designed for high-density slots. By utilizing ground tool-steel push blades with micro-polished finishes and progressive two-stage wedge pushers, our machines achieve slot fill factors exceeding 78% without damaging the copper wire enamel or tearing slot liners.
Q4: What PLC and automation control systems are standard on Nakro stator lines?
While our standard configuration integrates high-performance Siemens S7-1200/1500 or Omron Sysmac PLCs paired with digital touchscreens, we regularly customize controller packages for European requirements, including Beckhoff TwinCAT EtherCAT architectures, Schneider Electric components, and SEW-Eurodrive servo systems. All interfaces include full English language navigation and OPC UA industrial communication protocols.
Q5: What are the standard shipping arrangements and Incoterms for delivery to the Port of Turku?
We routinely ship on CIF Port of Turku, CIP Helsinki, or FOB Ningbo/Shanghai terms. Equipment is packaged in vacuum-sealed anti-corrosion barrier foil, treated with silica gel desiccant packs, and crated in fumigated ISPM-15 compliant seaworthy wooden cases engineered to withstand the North Sea and Baltic maritime transport routes.
Q6: How is equipment installation, commissioning, and staff training handled in Southwest Finland?
Nakro provides a flexible two-tier commissioning program: (1) On-site deployment of our senior electrical and mechanical field engineers to supervise machine positioning, wiring hookup, tooling calibration, and operator/maintenance training directly on your factory floor; or (2) Comprehensive remote FAT video sign-off backed by live VPN remote-access commissioning support, comprehensive English operation manuals, and step-by-step HD video procedures.
Q7: Can we also source matched motor components (magnets, commutators, brushes) directly through Nakro?
Yes, this is one of Nakro's core competitive advantages. Beyond supplying machinery, we supply precision hook commutators, planar commutators, slip rings, high-permeability N52 NdFeB magnets, ferrite arc segments, and graphite carbon brushes. This one-stop approach ensures that your raw parts and automated assembly tooling interface with flawless dimensional compatibility.
Q8: What is the typical equipment lead time from drawing sign-off to shipment?
Standard stand-alone machines (such as single-operator coil inserters or needle winders) typically have a production lead time of 45 to 60 days. Fully customized turnkey stator production assembly lines with automated conveyors and end-of-line testing benches are engineered, assembled, and run-off within 90 to 120 days depending on tooling complexity.
Q9: How does Nakro prevent wire insulation scraping during the insertion cycle?
Nakro insertion tooling utilizes mirror-polished Cr12MoV / SKD11 alloy guide blades hardened to HRC 60-62. The synchronized motion of the push fingers and wedge pusher guarantees that the wire bundles slide parallel along the slot axis without friction points against the sharp laminated iron edges of the stator core.
Q10: What spare parts inventory is recommended for continuous production runs in Finland?
With every machine delivery, Nakro includes an essential 1-to-2 year wear parts package: spare winding needles/flyers, inserting blades, wedge cutoff knives, pneumatic seal kits, and spare proximity sensors. Additional replacement parts are maintained in stock for rapid dispatch via DHL/FedEx air freight to Turku within 3 to 5 business days.
Accelerate Your Stator Automation Project for the Turku Market
Submit your stator lamination drawings (PDF/DWG), slot parameters, and required output targets. Nakro's engineering team will deliver a comprehensive proposal with station layout, cycle time simulation, tooling design, and formal quotation within 48 hours.
