High-Efficiency Stator Insertion Equipment & Motor Accessories
Explore our core portfolio of CE-compliant coil winding machines, automated stator insertion systems, high-precision commutators, and electromagnetic materials engineered for demanding production environments.

DC Motor Armature Collector Slip Ring Commutator NDPJ-HXQ
High-precision commutator with integrated rotor stator fan assembly. Engineered with high-grade copper alloys to withstand high rotational speeds and severe thermal stresses.
- Model: NDPJ-HXQ
- High-Dielectric Mold
- Minimal Runout

Automatic EV New Energy Motor Stator Production Line
Full automated hairpin and distributed stator manufacturing system for EV traction motors. Dual 220V/380V compatibility with integrated slot paper forming and laser welding.
- Hairpin / Wire Inserter
- CE Certified
- Zero-Damage Tooling

PLC Controlled Cooler Motor Stator Coil Winding Machine
High-speed CNC coil winder tailored for evaporative cooler and HVAC fan motor stators. Delivers ultra-uniform coil grouping and neat transfers directly to inserting magazines.
- PLC Programmed
- Multi-Spindle Axis
- Active Tensioning

PLC Controlled Armature Rotor Winding Equipment
Heavy-duty flyer winder for universal armatures and vehicle starter motors. Equipped with premium engine and servo drives, backed by a comprehensive one-year warranty.
- 1 Year Warranty
- High Dynamic Speed
- Commutator Indexing

Copper Hook Commutator Armature NDPJ-HXQ-871A
Custom-engineered automotive DC motor commutator with copper collector hooks. Provides optimal fusing performance for wiper motors, cooling fans, and window lifters.
- Model: NDPJ-HXQ-871A
- Electrolytic Copper
- High Centrifugal Limit

24-Segments Hook Type Commutator NDPJ-HXQ-640A
Precision 8.4*25*16 commutator designed for angle grinders and high-RPM power tools. Highly resistant to electrical arc erosion and excessive commutator bar wear.
- 24 Segment Profile
- Size: 8.4*25*16 mm
- Low Sparks / Long Life

N52 Neodymium Rare Earth Block Magnet NDPJ-CW-61
Ultra-high remanence grade N52 sintered NdFeB rectangular magnet blocks. Tailored for permanent magnet synchronous motors (PMSM) and BLDC industrial servo drives.
- Grade: N52 NdFeB
- High Thermal Coercivity
- Anti-Corrosion Ni-Cu-Ni

Automobile Carbon Brush Parts NDPJ-TS-1
Advanced metallized graphite electrical brushes delivering minimal voltage drop, low acoustic noise, and extreme service durability for automotive accessory motors.
- Model: NDPJ-TS-1
- Optimal Conductivity
- Low Friction Ratio
Stator Coil Insertion Line Architecture: Physics, Kinematics, and Quality Assurance
In modern industrial motor production—spanning IEC standard induction frames, BLDC compressor stators, and advanced traction motors—the coil and wedge insertion phase constitutes the single greatest mechanical risk to insulation integrity and slot copper packing density.
Simultaneous Coil & Wedge Synchrony
Traditional pneumatic insertion causes uneven mechanical stress, resulting in wire crossover pinching. Our CE-certified architecture employs independent AC servo actuators for the wire pushing foot and the slot wedge feed magazine.
- Positional repeatability within ±0.01mm
- Elimination of wedge buckling during insertion
- Real-time force feedback monitoring prevents wire severance
Guide Blade Metallurgy & Slot Dynamics
The insertion tooling blades guide individual copper conductors through narrow slot openings without scraping the dielectric enamel coating. We utilize imported Swedish powder metallurgical tool steels (Vanadis/ASP23) hardened to HRC 62-64.
- Surface roughness polished to Mirror Ra ≤ 0.05μm
- Specialized PVD titanium carbonitride (TiCN) coating
- Minimizes friction coefficients down to μ < 0.12
Dielectric Enamel Protection Protocols
Electrical failure in inverter-driven motors frequently originates from microscopic enamel scratches incurred during insertion. Our insertion lines integrate progressive expansion blades that prevent wire crossing at tooth tips.
- Zero micro-crack guarantee on Class H & C enamels
- Continuous slot liner cuff protection tooling
- Prevents partial discharge inception voltage (PDIV) drops
| Performance Dimension | Legacy Hydraulic / Pneumatic Inserters | Nakro Full Servo-Electric Automated Lines | Engineering Benefit |
|---|---|---|---|
| Slot Fill Factor Capability | Maximum 68% - 72% net copper fill | Up to 82% net copper slot fill | Higher torque density and IE4/IE5 energy compliance |
| Cycle Time (36-Slot Stator) | 28 to 38 seconds per cycle | 12 to 18 seconds (including wedge indexing) | More than 110% throughput surge per operator shift |
| Tooling Changeover Duration | 4 to 6 hours (manual mechanical alignment) | ≤ 25 minutes (modular quick-clamp system) | High flexibility for mixed-model batch manufacturing |
| Wire Insulation Damage Rate | Typically 0.4% - 1.2% requiring rework | ≤ 0.02% scrap / surge test rejection | Preserves enamel film integrity against VFD inverter surges |
| Wedge Material Adaptability | Limited to rigid pressboard or DMD | Nomex, DMD, NMN, Polyimide, Magnetic Wedges | Fully supports thermal Class B, F, H, and EV applications |
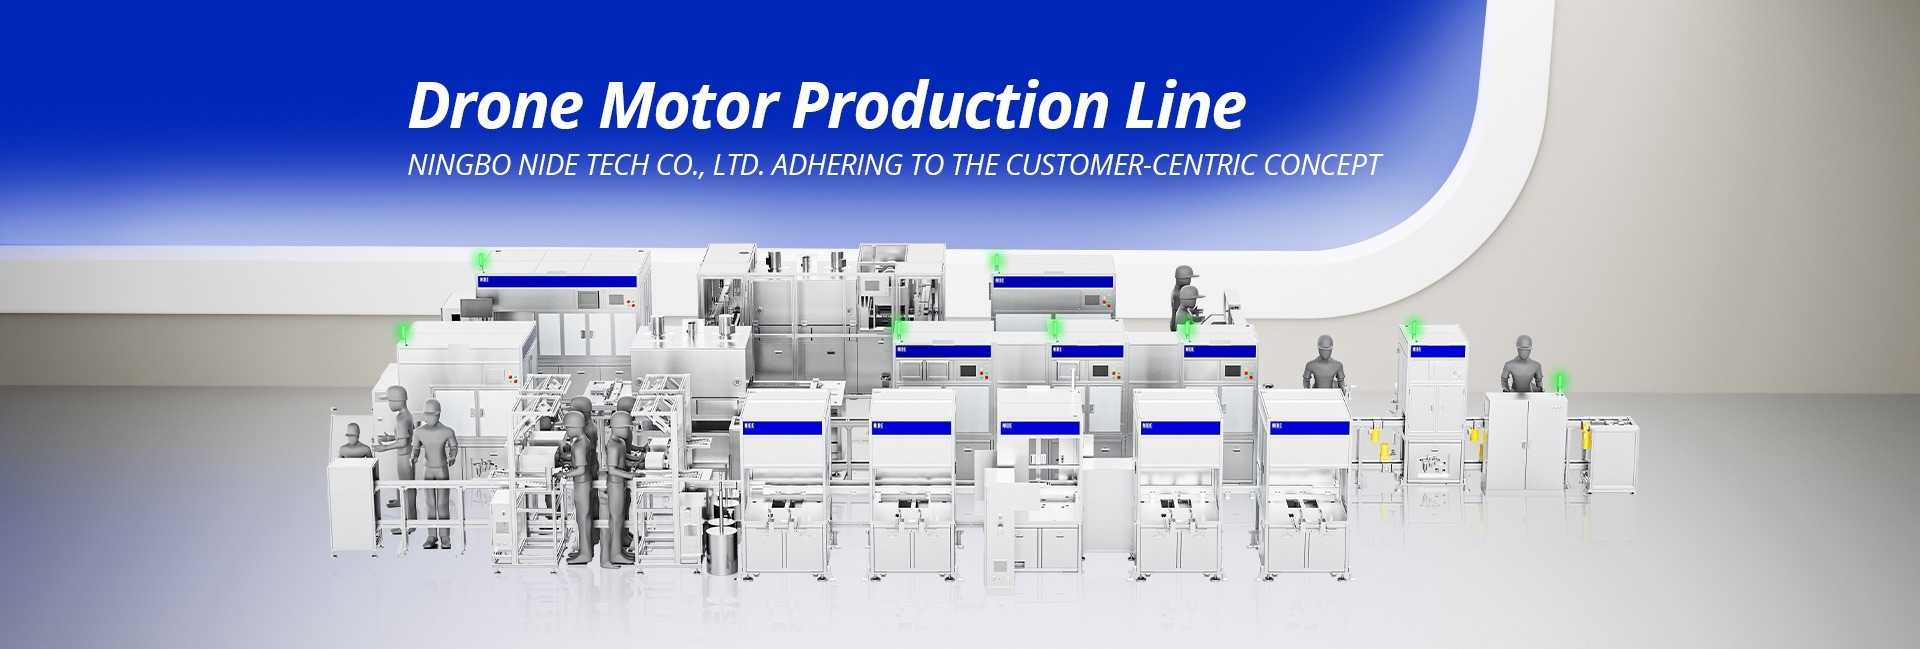
Mitigating Radial Slot Stress and Wedge Displacement
During the insertion stroke, the coil conductors must pass through the slot opening (isthmus) which is often narrower than the aggregated diameter of the coil bundle. Without controlled multi-stage guide teeth, conductors experience acute shear stress, leading to strand thinning and copper work hardening.
Nakro insertion machines solve this challenge by integrating servo-driven counter-push mechanisms. As the lower pusher advances the coils upward, an overhead servo retainer applies controlled descending pressure against the coil crowns. This stabilizes the coil loop shape, eliminates flaring, and ensures uniform end-turn geometries ready for intermediate lacing.
Contact UsWhy Tier-1 Motor Manufacturers Source from Ningbo Nakro
Combining 14+ years of specialized motor manufacturing machinery expertise with complete motor component manufacturing, Nakro is the single-source partner for turnkey industrial automation.
ISO 9001 & CE Verified Standards
All machinery conforms strictly to the European Union Machinery Directive 2006/42/EC and Low Voltage Directive 2014/35/EU, equipped with multi-channel safety relays, light curtains, and ergonomic interlocks.
Global Export in 50+ Nations
Over 13 years of direct machine export footprint across Southeast Asia, Eastern Europe, South America, and the Middle East, supported by on-site field engineers and localized service partners.
Proprietary In-House Tooling R&D
We do not outsource critical tooling. Precision blade grinding, wire transfer pushers, and wedge forming dies are custom-machined in our 30,000+ m² production facility using multi-axis CNC wire-EDM.
Holistic Motor Supply Ecosystem
Beyond automation, we supply precision commutators, rare-earth NdFeB magnets, carbon brushes, and insulation materials, ensuring your tooling is pre-validated with actual production components.
Pre-Shipment Run-Off Acceptance
Every line undergoes rigorous dry-cycle testing and hot-testing utilizing your supplied iron cores and magnet wire. We deliver detailed Cpk analytical reports and video verifications prior to crate dispatch.
Turnkey Lifecycle Consultation
Our sales engineering division delivers comprehensive line layout planning, cycle time simulations, utility load calculations, operator training regimens, and preventive maintenance frameworks.
Next-Generation Technology Trends in Stator Insertion Lines
As the electric machinery industry undergoes a seismic shift driven by strict IE4/IE5 minimum energy performance standards (MEPS) and the proliferation of 800V EV traction motors, insertion line requirements are evolving rapidly.
Full Electronic Cam Drive Migration
Mechanical Geneva linkages and pneumatic pushers are being completely supplanted by programmable electronic multi-axis cams. This facilitates infinitely variable speed curves during the insertion stroke, decelerating exactly as the coils compress into the slot base to prevent tooth deflection.
Magnetic Slot Wedge Automated Feeding
To eliminate high-frequency harmonic iron losses in high-speed industrial drives, motor designs increasingly specify magnetic powder composite slot wedges. Nakro insertion tooling features specialized non-shattering feeding channels engineered for fragile magnetic wedge strips.
Smart Factory Edge & IoT Monitoring
Modern procurement executives demand real-time OPC-UA connectivity. Nakro lines feature integrated piezoelectric force transducers that plot the force-displacement curve of every insertion cycle, automatically segregating stators that exhibit abnormal frictional spikes.
Rapid Modular Tooling (<20 Mins)
Contract motor manufacturers face fragmented lot sizes. Future-ready insertion lines utilize servo-driven stack height adjustments directly from the touchscreen HMI, reducing lamination stack changeover time to minutes without mechanical teardowns.
Standardized Modular Engineering Across All Motor Families
Whether your manufacturing facility produces deep-submersible pump stators with extreme lamination stack heights exceeding 350mm, or fractional-horsepower hermetic refrigerator compressor stators requiring cycle times under 12 seconds, Nakro standardizes on rock-solid mechanical foundations.
Heavy stress-relieved steel machine bases prevent thermal and vibrational drift over millions of duty cycles. Standardized electrical cabinets utilize global-tier components (Mitsubishi, Siemens, Schneider, and SMC Pneumatics), guaranteeing spare part availability regardless of your global operational geography.
Contact Us
Frequently Asked Questions: Stator Coil Insertion Line Procurement
In-depth answers addressing mechanical tolerances, insulation safety, operational parameters, and overseas installation procedures.
What is the maximum achievable slot fill factor with Nakro servo insertion lines?
Under conventional single-phase or three-phase distributed winding topologies, Nakro automated servo coil inserting machines comfortably achieve between 78% to 82% slot fill factor (total bare copper area relative to net slot area after accounting for slot insulation paper). This is accomplished via multi-stage profile guide blades and high-precision CNC pre-winding grouping that organizes parallel wire bundles linearly, eliminating random crossovers prior to insertion.
How does the machine prevent enamel scraping on Grade 2 heavy-build magnet wire?
Enamel scratch prevention is achieved through three engineering barriers: First, the insertion guide blades are manufactured from vacuum-hardened Vanadis powder metallurgy steel with mirror hand-lapping to Ra ≤ 0.05μm, coated with TiCN for extreme lubricity. Second, the blade tips feature lead-in tapers that physically shield the stator tooth edges from contact with the entering conductors. Third, a pneumatic micro-lubrication system applies an atomized, residue-free vanishing lubricant to the wire bundle immediately prior to insertion, which evaporates completely during curing/varnishing.
Can a single machine accommodate different stator stack heights and slot numbers?
Yes. If the internal stator bore diameter and the slot count remain constant, accommodating different stack heights (e.g., from 40mm to 160mm) is completely digital: the operator simply inputs the new stack height on the HMI touchscreen, and the servo pusher stroke dynamically re-indexes without changing mechanical tooling. If the stator bore diameter or lamination slot geometry changes, a complete modular tooling cartridge changeover (including guide blades, pusher foot, and wedge guides) is required, which takes approximately 20 to 30 minutes via quick-release locating pins.
What insulation materials are compatible with the automatic wedge maker station?
The integrated automatic wedge cutting and feeding module processes a broad array of roll-fed electrical insulation materials, including DMD (Dacron-Mylar-Dacron), NMN (Nomex-Mylar-Nomex), pure Nomex 410, Polyimide film, and electrical-grade presspaper with thicknesses ranging from 0.15mm to 0.38mm. The station features precision servo feeding, heating/creasing wheels for profile shaping, and hardened tungsten carbide guillotine blades that ensure clean, burr-free wedge edges.
What are the typical CE compliance and safety mechanisms integrated into the line?
Our CE certification adheres fully to European Harmonized Standards including EN ISO 12100 (Risk Assessment & Reduction), EN 60204-1 (Electrical Safety of Machinery), and EN ISO 13849-1 (Safety-Related Parts of Control Systems, Category 4 / Performance Level e). The work envelope is guarded by Category 4 infrared safety light curtains, dual-channel emergency stop circuits with monitoring relays, pneumatic pressure decay dump valves, and interlocked transparent polycarbonate shields.
What factory acceptance testing (FAT) is conducted before export shipping?
Every machine undergoes a strict factory acceptance protocol: First, a continuous dry run of 50,000 cycles to confirm thermal stability of servo motors and mechanical linkages. Second, actual production hot-testing using 200 to 500 sets of customer-supplied stator laminations, slot paper, and magnet wire. We verify slot fill, end-turn height consistency, surge test withstand (≥ 3000V), insulation resistance (> 500MΩ), and ground hipot breakdown voltage. FAT video records and physical stator samples are dispatched to the client for final sign-off before seaworthy fumigated wooden crating.
What post-sales support and installation services are available globally?
Nakro provides comprehensive overseas commissioning and technical assistance. Our factory-certified field engineers conduct on-site installation, line integration, and operator training covering routine calibration, recipe setup, and preventive maintenance. Furthermore, all control panels include an industrial VPN gateway enabling remote telemetry, PLC diagnosis, and software updates over secure cloud connections, ensuring instant troubleshooting regardless of geographical time zones.
Upgrade Your Stator Production Line with CE-Certified Automation
Submit your stator lamination drawings (DWG/DXF/STEP), slot geometry, wire gauge bundle sizes, and target tact time. Our application engineering team will deliver a comprehensive proposal with complete cycle time simulations and line layout within 24 business hours.
